
How CO2 compression capacity shapes CCUS systems for cement plants




How CO2 Compression Capacity Shapes CCUS Systems for Cement Plants
For technical evaluators, CO2 compression capacity is a defining design variable in CCUS systems for cement plants. It determines how reliably captured flue-gas CO2 can be dehydrated, compressed, conditioned, and delivered to pipeline, shipping, utilization, or storage networks. Beyond nominal throughput, the selected capacity affects electrical demand, compressor redundancy, capture availability, emissions performance, and long-term project economics. The central question is not simply how many tonnes of CO2 a compressor can process per hour. It is whether the compression train can remain stable across the real operating envelope of a cement works.
Cement is a particularly demanding application because much of its CO2 arises from limestone calcination rather than fuel combustion. Even where alternative fuels, kiln efficiency measures, or electrification reduce combustion emissions, process emissions remain. Carbon capture can address that residual stream, but the value of capture depends on the plant’s ability to move CO2 from the capture island to an approved transport or storage route without creating an operational bottleneck.
In that context, compression is not a downstream utility to be sized after the capture technology has been selected. It is the interface between kiln operations, solvent or oxyfuel systems, dehydration, transport specifications, and the commercial terms of an offtake agreement. A train that is undersized, poorly turndown-capable, or designed around an unrealistic feed-gas assumption can erode the availability of the entire CCUS system for cement plants.
Capacity begins with the operating profile, not annual capture ambition
Annual capture targets are useful for planning, but compressors do not operate on annual averages. They see hourly flow, inlet pressure, temperature, moisture, impurity concentration, and variability caused by kiln conditions. A cement plant may operate close to a steady thermal load for long periods, yet raw mill operation, fuel changes, kiln trips, maintenance shutdowns, bypass flows, and capture-unit regeneration cycles can still alter the CO2 stream presented to the compression system.
A sound capacity basis therefore separates at least three conditions: normal operation, high-flow operation, and low-load or transient operation. The normal case establishes expected energy use. The high-flow case tests whether the train can handle periods when captured CO2 exceeds the nominal design rate. The low-load case is equally important, particularly where a compressor has surge constraints or where a liquefaction and shipping chain requires relatively stable feed conditions.
Design teams sometimes make the opposite mistakes. Oversizing can increase capital cost and reduce part-load efficiency. Undersizing may appear economical at first, but it forces capture curtailment whenever kiln output or capture performance rises above the assumed average. If the project is assessed against a contracted storage volume or an emissions-performance threshold, routine curtailment is not a minor inconvenience; it may alter the business case.
The mass balance must be based on captured CO2, not kiln emissions alone
The starting point should be a reconciled mass balance extending from stack gas through capture, purification, dehydration, compression, intermediate storage where applicable, and the export battery limit. Gross kiln emissions are only one input. The compressor capacity must reflect the actual mass of CO2 delivered by the capture process, including expected capture rate, process losses, recycle streams, startup behavior, and planned maintenance arrangements.
This distinction becomes material when evaluating different capture routes. Post-combustion systems may produce a CO2-rich stream that requires significant dehydration and impurity management. Oxyfuel configurations may offer a different composition profile but still demand careful handling of non-condensables and contaminants. Calcium looping, adsorption, membrane systems, and hybrid schemes each create their own integration questions. Compression capacity cannot be properly specified as an isolated number without a defined inlet-gas envelope.
Pressure destination changes the entire compression problem
The required export condition drives equipment architecture. A CO2 stream destined for a dense-phase pipeline is not conditioned in the same way as CO2 intended for temporary liquid storage and marine transport. Nor is either identical to a lower-pressure utilization route. The destination defines final pressure, temperature limits, allowable water content, impurity tolerances, metering requirements, and the consequences of an off-spec event.
For pipeline transport, phase behavior deserves early attention. CO2 mixtures do not behave exactly like pure CO2, and even relatively small quantities of nitrogen, oxygen, argon, hydrogen, sulfur compounds, or water can affect density, corrosion risk, compression power, and the pressure-temperature envelope. A transport operator may impose its own specification, often more decisive than a generic design assumption. The capture provider, compressor vendor, pipeline developer, and storage operator must use a common composition basis.
Shipping adds another layer. If liquid CO2 is stored between compression and vessel loading, the project needs to account for buffer capacity, refrigeration or cooling requirements, loading schedules, boil-off management where relevant, and the practical consequences of a missed vessel slot. Compression capacity may need to support a loading window rather than merely match average capture output. That can favor a different combination of compression, liquefaction, and storage than a direct pipeline connection.
Dehydration is inseparable from compression
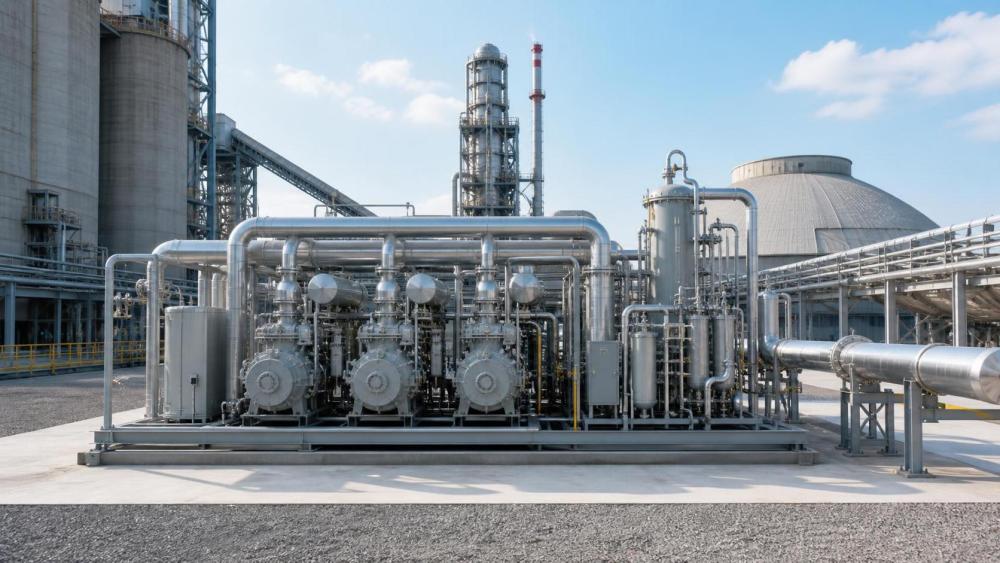
Water control is one of the clearest examples of why nameplate flow is not enough. Free water in a CO2 system can lead to corrosive conditions, operational instability, and, under certain pressure-temperature conditions, hydrate concerns. The acceptable moisture level should be derived from the selected transport route, materials, operating conditions, and contractual specification. It should not be treated as a generic vendor preference.
The dehydration unit must also be designed for realistic inlet conditions. If upstream cooling, knockout, or capture operations allow water carryover beyond the assumed level, a downstream molecular sieve or other drying system may experience shorter cycles, higher regeneration duty, or premature loss of performance. Evaluators should ask whether the stated compressor capacity remains valid at the maximum expected humidity and impurity load, rather than only at clean, dry design conditions.
Compression power can reshape the plant electrical strategy
CO2 compression is commonly among the major electrical loads in a cement CCUS project. The exact duty depends on inlet pressure, discharge pressure, gas composition, interstage cooling, compressor technology, flow variability, and the required conditioning route. It should therefore be assessed alongside capture regeneration energy, cooling demand, flue-gas fans, oxygen production where applicable, and site electrical constraints.
A technically feasible compressor can still become a project constraint if the cement plant’s electrical connection, internal substations, backup arrangements, or planned renewable power supply cannot support its operating profile. This is particularly relevant where CCUS is phased in. A first capture train may be built around existing electrical capacity, while later expansion requires a new grid connection or a redesigned power distribution system. Leaving that dependency until late engineering usually narrows the available options.
Intercooling and heat recovery also merit practical scrutiny. Interstage cooling reduces compression work and protects equipment, but it adds cooling-water or air-cooling infrastructure. Recovered heat may have value, yet its temperature level, reliability, and seasonal fit with plant demand need to be demonstrated. It is better to treat recoverable compression heat as a possible integration benefit than to rely on it prematurely in the core energy balance.
Availability is designed through trains, controls, and maintainability
Compression availability is often discussed as a vendor reliability figure. In practice, it is a system property. A highly reliable compressor does not solve the problem if upstream dehydration has no bypass strategy, if a critical cooler cannot be isolated, or if an off-spec CO2 event forces a lengthy restart. The question for evaluators is how the full conditioning and compression block behaves when something predictable goes wrong.
One large train can reduce equipment count, but it may create a single point of failure. Multiple trains can improve operational flexibility and allow maintenance without complete capture interruption, although they introduce more valves, controls, and interfaces. There is no universal preference. The decision should reflect the kiln’s operating pattern, the consequences of venting or curtailing captured CO2, spare-parts lead times, site maintenance capability, and the tolerance of the transport system for variable receipts.
Turndown performance should receive the same attention as maximum capacity. Anti-surge control, recycle arrangements, startup sequencing, and compressor protection logic need to work with the capture plant rather than against it. If the capture process temporarily produces less CO2, the compression train should not consume disproportionate energy through recycling or force unnecessary capture shutdowns. Dynamic studies may be warranted where the site expects frequent load changes, shared export infrastructure, or constrained intermediate storage.
Materials and impurities deserve an early technical review
Cement-derived CO2 can contain impurities that matter to both equipment integrity and transport acceptance. The relevant species depend on fuel mix, raw materials, capture method, flue-gas treatment, and upstream polishing. Oxygen, nitrogen, sulfur compounds, nitrogen oxides, particulates, amines or solvent degradation products, and residual moisture should be examined against the selected process route. Their importance is not limited to corrosion. They can affect phase behavior, compressor internals, seals, dehydration performance, and downstream storage compatibility.
Material selection should follow a documented corrosivity assessment rather than a broad assumption that dry CO2 is benign. Transient conditions matter: startup, shutdown, upset cooling, water breakthrough, and temporary off-spec gas may create a more severe environment than steady-state operation. This is also where clear battery limits matter. If the capture supplier guarantees a composition at one point and the transport operator requires another at a later point, the owner must establish who is responsible for the intervening conditioning duty.
Standards establish discipline, but they do not replace project-specific specifications
There is no single standard that fully defines a cement CCUS compression system. The applicable framework usually combines local pressure-equipment and machinery regulations, process safety requirements, electrical standards, piping codes, transport-network specifications, and storage-permit conditions. ISO 27913 provides a useful reference point for CO2 pipeline transportation systems, while ISO 27914 addresses geological storage concepts and operations. Their application must be confirmed against the project jurisdiction and contractual structure.
Mechanical integrity typically requires careful alignment among compressor package requirements, piping design, pressure-relief philosophy, hazardous-area classification where applicable, instrumentation, and emergency shutdown logic. A project may also draw on established engineering codes such as ASME or EN-based frameworks, depending on location and owner requirements. The key is traceability: each design condition, material decision, relief case, and export-quality limit should be linked to an approved basis of design.
This discipline is central to the broader benchmarking approach of the Global Hydrogen-Economy & Zero-Carbon Infrastructure (G-HEI). Its work spans CCUS alongside electrolysis, cryogenic hydrogen logistics, hydrogen-ready generation, and high-pressure refueling. Standards such as ISO 19880, ASME B31.12, and SAE J2601 are particularly relevant to hydrogen infrastructure rather than direct substitutes for CO2 compression requirements. Their inclusion in a cross-sector technical framework is valuable because it reinforces a necessary principle: high-pressure decarbonization assets require rigorous control of materials, interfaces, operating envelopes, and verification evidence.
A practical evaluation sequence
Before selecting a compression configuration, a technical review should establish a few non-negotiable inputs. These are more useful than asking suppliers for an early headline capacity:
- Hourly and seasonal CO2 flow envelopes from the selected capture process, including startup, shutdown, and upset scenarios.
- A validated inlet composition range, with clear assumptions for moisture and contaminants.
- The final delivery condition and quality specification issued by the pipeline, shipping, utilization, or storage counterparty.
- Site electrical, cooling, plot-space, noise, lifting, maintenance, and spare-parts constraints.
- Required capture availability, permitted curtailment, and the commercial consequence of failing to deliver CO2.
With those inputs in place, evaluators can compare single-train and parallel-train concepts, assess energy at realistic operating points, test transient behavior, and define where contingency capacity is justified. The result is not merely a better compressor specification. It is a more credible interface between a cement plant’s decarbonization plan and the infrastructure needed to transport or permanently store its captured CO2.
For cement projects moving from concept selection into FEED, the most productive next step is usually a joint review of the capture mass balance, export specification, and operating philosophy. Compression capacity should then be set against the whole chain—not against a single annual emissions figure—because that is where the practical resilience of CCUS systems for cement plants is decided.
Related News
- How CO2 compression capacity shapes CCUS systems for cement plantsAug 30, 2026CCUS systems for cement plants depend on the right CO2 compression capacity. Explore design, energy, reliability, and transport factors for resilient projects.
- When does refinery decarbonization investment pay off for aging assetsAug 17, 2026Refinery decarbonization investment pays off when aging assets cut carbon, energy, and compliance costs while protecting margins. See the key payback drivers and strategic timing.
- What Delays CCUS Infrastructure Projects Most: Permitting, CO2 Transport, or Storage Readiness?Aug 11, 2026CCUS infrastructure projects often stall on storage readiness before permitting or CO2 transport. Learn which bottleneck delays projects most and how to reduce schedule risk faster.
- How to Compare CCUS Systems Manufacturers for Industrial CO2 ProjectsJul 12, 2026CCUS systems manufacturers vary widely in process fit, reliability, and lifecycle risk. Learn how to compare suppliers for industrial CO2 projects and choose a bankable, integration-ready solution.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Elena Carbon
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.