
Metal Fabrication for Cryogenic Systems: Tolerance Mistakes to Avoid




In cryogenic hydrogen infrastructure, tolerance errors rarely stay small. A flange face that looks acceptable at ambient temperature can distort at liquefied-gas conditions, opening a path to leakage, insulation loss, or premature fatigue. That is why metal fabrication for cryogenic systems demands tighter dimensional discipline than many conventional industrial assemblies.
The issue matters even more in the 2026 hydrogen buildout. Large-scale electrolysis, liquid hydrogen logistics, hydrogen-ready turbines, CCUS assets, and 70MPa refueling networks are moving from pilot projects to strategic infrastructure. In that setting, tolerance control is not a workshop detail. It affects compliance, commissioning speed, lifecycle cost, and asset security.
Why cryogenic tolerance control is a project-level concern
Cryogenic service changes how metal behaves. Materials contract, seals respond differently, weld zones carry residual stress, and stacked tolerances become more visible during cooldown. A dimension that passes inspection at room temperature may still fail in service.
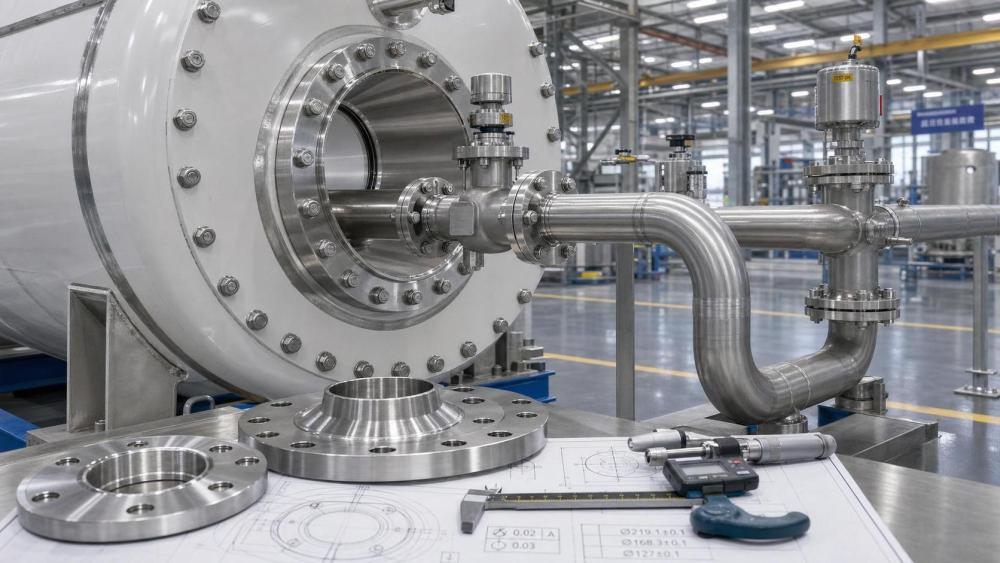
For metal fabrication tied to hydrogen systems, the risk extends beyond rework. Misalignment can interrupt vacuum integrity, raise boil-off losses, complicate maintenance access, and trigger nonconformance against standards-driven acceptance criteria.
This is one reason technical benchmarking groups such as G-HEI place so much weight on material integrity and fabrication quality. In sovereign-scale decarbonization programs, fabrication tolerance becomes part of infrastructure resilience, not just manufacturing quality.
What tolerance really means in cryogenic metal fabrication
Tolerance is often treated as a drawing note. In practice, it is the allowable dimensional variation across the whole assembly path, including cutting, forming, machining, welding, fit-up, post-processing, transport, and installation.
For cryogenic metal fabrication, the critical question is not only whether a part meets nominal dimensions. The more useful question is whether the final assembly will maintain sealing, structural stability, and thermal performance after repeated cold cycles.
That broader view matters for vacuum-insulated vessels, transfer lines, valve bodies, supports, nozzle penetrations, and pump housings. Each part may look manageable on its own. The failure usually appears when multiple “acceptable” deviations accumulate.
Tolerance is functional, not only geometric
A flatness issue can become a sealing problem. A bore position error can create shaft misalignment. A nozzle offset can load connected piping beyond design assumptions. Good metal fabrication for cryogenic duty translates dimensions into operating consequences.
Tolerance mistakes that create the most trouble
Not every deviation carries the same risk. The most expensive failures usually come from a short list of recurring mistakes, especially where fabrication and field installation teams work from different assumptions.
Ignoring thermal contraction during design handoff
This is a classic gap between design intent and fabrication execution. Dimensions may be checked at ambient conditions without confirming how the assembly will behave at cryogenic temperature. Stainless steels, nickel alloys, and mixed-material interfaces do not shrink uniformly.
When that is missed, bolt preload changes, seal compression shifts, and sliding supports can bind. The drawing may be correct. The fabricated outcome is still wrong for the operating state.
Treating weld distortion as a finishing issue
In cryogenic metal fabrication, weld distortion is rarely cosmetic. It changes face runout, concentricity, straightness, and mating geometry. If correction happens too late, machining stock disappears, repair welding increases, and qualification records become harder to defend.
Using general industrial tolerances for critical interfaces
Cryogenic vessels and piping often contain a few dimensions that deserve much tighter control than the rest of the assembly. Problems arise when a blanket tolerance is applied across components with very different functional sensitivity.
Examples include sealing lands, valve seats, jacket annulus spacing, nozzle orientation, and instrument penetrations. Metal fabrication plans should distinguish routine dimensions from function-critical ones.
Overlooking tolerance stack-up across suppliers
Hydrogen projects rarely come from one shop. Fabricated spools, skids, valve packages, supports, and insulated assemblies often arrive from different locations. Each supplier may meet its own drawing, while the combined assembly still misfits.
That is where project delay begins. Installation crews start modifying supports, slotting holes, or forcing alignment. In cryogenic service, those field fixes can undermine design margins.
Where these mistakes show up most often
Some components deserve earlier review because they combine thermal sensitivity, sealing demands, and fabrication complexity. They also sit at the center of hydrogen logistics and storage performance.
From a broader infrastructure view, these are not isolated shop-floor defects. They affect uptime in liquid hydrogen logistics, interface quality in refueling systems, and reliability across adjacent zero-carbon assets benchmarked against ISO 19880, ASME B31.12, and related frameworks.
How to reduce tolerance failures before fabrication starts
The most effective control point is earlier than many schedules assume. Once material is cut and welded, options narrow quickly. Better metal fabrication outcomes usually come from a stronger pre-release process rather than heavier final inspection.
Define critical-to-function dimensions separately
Drawings should clearly identify which dimensions affect sealing, cold movement, load transfer, or vacuum performance. Those dimensions need different review attention, measurement plans, and acceptance logic than cosmetic or low-risk features.
Link tolerances to process capability
A tolerance that looks sensible in design software may be unrealistic for the chosen cutting, forming, or welding route. Good metal fabrication planning checks capability before release, not after the first nonconforming batch.
Use staged dimensional verification
Inspection should follow the risk sequence of the build. Verify incoming material, pre-weld fit-up, post-weld distortion, final machining, and assembly interfaces. Waiting until the end hides the root cause.
- Check datum strategy before fabrication begins.
- Measure interfaces after each distortion-driving operation.
- Confirm cold-service assumptions during design review.
- Align supplier inspection reports to one dimensional baseline.
Decision points that deserve closer review
Some tolerance questions appear late because they are treated as fabrication details. In reality, they deserve management attention early, especially when schedule pressure encourages drawing release before interface alignment is finished.
Material combinations and joining method
Different alloys respond differently to welding heat and cryogenic contraction. A metal fabrication plan for austenitic stainless steel may not transfer cleanly to aluminum, nickel alloy, or dissimilar-metal joints.
Inspection method versus acceptance requirement
If the acceptance window is tight, the measurement method must match. Tape-and-rule checks cannot support high-consequence interfaces. Laser measurement, CMM verification, or fixture-based checks may be justified by the rework they prevent.
Transport and site handling effects
Large cryogenic assemblies can move out of tolerance after fabrication through lifting, vibration, or temporary support removal. Final dimensional acceptance should reflect delivered condition, not only shop release condition.
A practical way to apply this in hydrogen projects
For zero-carbon infrastructure, the useful approach is to connect metal fabrication tolerances to system-level risks. Start with the interfaces that can stop commissioning, compromise containment, or increase lifecycle energy loss.
Then compare drawing intent, supplier process capability, inspection evidence, and installation assumptions. Where those four do not align, tolerance risk is already present, even before the first weld arc starts.
That review is especially relevant for projects aligned with G-HEI priorities, where cryogenic liquid hydrogen logistics and related assets are benchmarked against demanding international standards and long-term performance expectations.
The next sensible step is to build a short tolerance register for each critical assembly: key dimensions, cold-service assumptions, inspection method, responsible supplier, and hold points for release. That creates a clearer basis for design review, supplier comparison, and site readiness before errors become structural.
Related News
- Hydrogen Logistics for Export Terminals: Key Storage and Transfer RisksJul 11, 2026Hydrogen logistics for export terminals explained: discover key storage and transfer risks, from boil-off and embrittlement to ESD failures, and learn how stronger projects improve safety and bankability.
- Hydrogen Export Projects: Key Risks in Storage and ShippingJul 05, 2026Hydrogen export projects face critical storage and shipping risks, from boil-off and embrittlement to port bottlenecks and compliance. Learn how to assess bankable, scalable export chains.
- Metal Fabrication for Cryogenic Systems: Tolerance Mistakes to AvoidJul 01, 2026Metal fabrication for cryogenic systems demands precision. Learn the tolerance mistakes that cause leaks, distortion, and costly hydrogen project delays—and how to prevent them.
- Hydrogen Expo Closes With Norway Interest in Chinese Helium LiquefierJun 25, 2026Hydrogen Expo highlights Norway’s interest in a Chinese helium liquefier for liquid hydrogen logistics. Explore what this means for cryogenic equipment, standards compliance, and global project opportunities.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Marcus Valve
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.