
How Tank Material and Capacity Affect Distillery Fermentation Performance




Fermentation losses in a distillery are often blamed on yeast strain, temperature control, or recipe consistency. Yet the vessel itself can quietly shape the outcome just as much. Tank material affects heat transfer, sanitation, corrosion behavior, and flavor risk. Tank capacity changes hydrostatic pressure, cooling demand, fill-level flexibility, and the way a batch responds to process variation. For technical evaluators, these are not secondary details. They influence attenuation stability, cleaning frequency, product consistency, and the practical operating window of the fermenter.
When buyers compare fermentation systems, the first useful question is not simply how many liters a tank can hold. It is whether the vessel design matches the intended spirit, the fermentation profile, and the plant’s operating pattern. A tank that works well for one distillery may create avoidable instability in another if batch size, wash composition, ambient conditions, or cleaning discipline are different.
Why material choice changes fermentation behavior
Tank material is sometimes treated as a durability issue only, but in fermentation it also affects microbial control and thermal response. Distillation can remove many unwanted compounds later in the process, but unstable fermentation still creates downstream problems: foaming, stuck ferments, off-aromas, inconsistent alcohol yield, and more difficult cuts during distillation.
Stainless steel remains the default choice in many distillery environments because it combines chemical resistance, relatively easy cleaning, and a surface that can be finished to support hygienic operation. In practice, the value is not only that stainless steel is “clean.” The more important point is repeatability. A smooth, properly fabricated interior is less likely to trap solids, support localized contamination, or develop cleaning blind spots around welds and fittings. In a facility running frequent batches, that repeatability usually matters more than any single theoretical material advantage.
Material selection also affects how quickly a tank gains or loses heat. Fermentation is exothermic. If a vessel cannot release heat in a controlled way, the temperature gradient inside the tank may widen, especially in larger volumes or in plants with limited agitation. Yeast may then perform differently at the top and bottom of the vessel. That can show up as uneven sugar depletion, variable ester formation, or a narrower process margin during warm weather.
Surface condition matters as much as base material
Technical buyers sometimes focus on metal grade while paying less attention to finish quality and fabrication details. In fermentation service, internal weld quality, dead-leg control, nozzle arrangement, drainage geometry, and passivation can matter just as much as the nominal material itself. A well-specified stainless tank with poor internal finishing can be harder to sanitize than a simpler vessel built with better hygienic discipline.
This is why purchase review should include more than a material certificate. Buyers usually benefit from checking:
- whether internal welds are smooth and accessible for cleaning,
- whether the bottom geometry drains fully after CIP and rinsing,
- whether connections, ports, and manways create residue traps,
- whether gaskets and valves are suitable for ethanol-adjacent service and cleaning chemicals.
Comparing common material considerations in distillery use
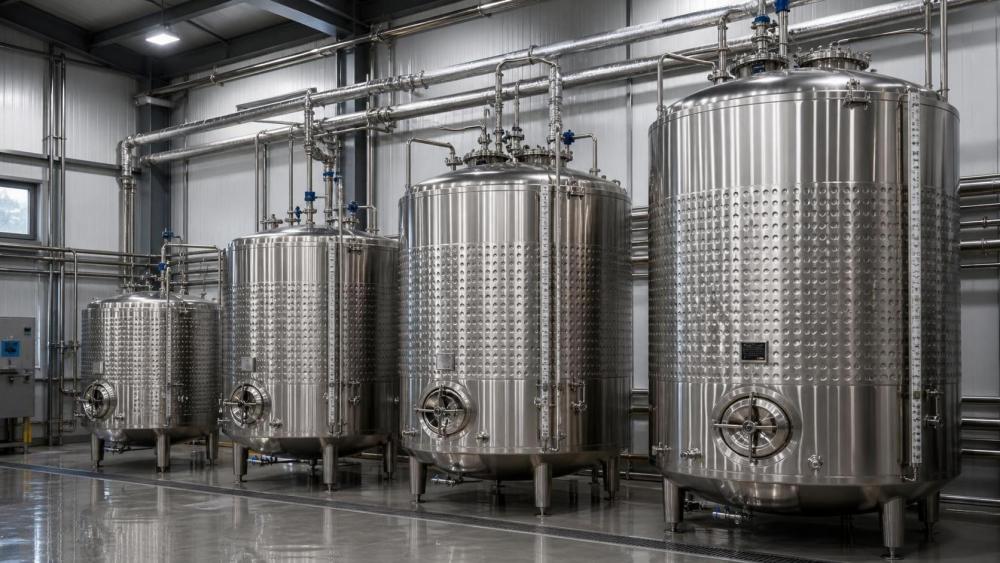
For buyers reviewing distillery fermentation tanks, these fabrication details often deserve equal weight with nominal volume. A 10,000 L vessel, for example, may look appropriate on paper, but if the cooling jacket coverage is limited or the bottom drain leaves residue behind, the operating burden can be higher than expected.
Capacity affects more than production throughput
Capacity is usually discussed in terms of output planning, but fermentation performance is sensitive to scale. A tank’s working volume changes the physical conditions experienced by the yeast. As tanks get larger, hydrostatic pressure rises at the bottom, heat removal becomes more demanding, and the penalty for a process deviation increases because more product is tied to a single batch.
That does not mean larger tanks are inherently worse. In many plants they are the most practical route to labor efficiency and floor-space utilization. The issue is that scale changes the control problem. The larger the tank, the more buyers need to evaluate whether instrumentation, jacketing, cleaning access, venting, and process flexibility have scaled with it.
Hydrostatic pressure and yeast stress
In taller vessels, pressure at the bottom of the fermenting liquid is greater. Depending on the fermentation style and yeast behavior, that may influence yeast activity, gas release, and the way solids settle or remain suspended. In some spirit applications the effect may be manageable, but technical teams should still account for vessel aspect ratio rather than focusing on total liters alone. Two tanks with the same nominal capacity can perform differently if one is tall and narrow while the other is shorter and wider.
This becomes relevant when a distillery is trying to preserve a familiar fermentation profile while increasing batch size. If the new vessel geometry changes pressure distribution and heat transfer behavior, matching the previous sensory result may require more than copying the recipe and fermentation time.
Cooling load and temperature gradients
As capacity increases, heat generated by fermentation becomes harder to remove uniformly. Cooling limitations can create hot zones, especially near the vessel core or in areas with weaker circulation. If the temperature sensor is placed in a more stable region, operators may not see the full extent of the variation. The result can be misleadingly acceptable control data paired with inconsistent fermentation behavior.
Buyers should therefore review not just whether a tank has a cooling jacket, but how much of the shell is jacketed, whether the cooling zones can be controlled independently, and whether the utility system can support peak heat removal. A large fermenter connected to an undersized chilled-water loop may be technically installed yet operationally constrained.
Working volume is the real operating figure
Nominal capacity is often not the same as usable fermentation capacity. Distillery washes can foam, generate CO2 rapidly, and require headspace for safe operation. If a 10,000 L tank can only be run comfortably at a much lower fill level under a given recipe, then the apparent capacity advantage narrows.
That is why buyers should ask for working volume assumptions, not only total volume. Headspace requirements vary with grain solids, nutrient additions, fermentation rate, and anti-foam strategy. A vessel that seems oversized may actually be correctly matched once foam behavior and cleaning access are considered.
Part-load operation is another overlooked factor. Some distilleries do not run every fermenter at full fill on every cycle. Seasonal demand, trial runs, or variable mash output may require lower loads. A tank that performs well only near full volume can be awkward in plants that need batch flexibility. Sensor position, cooling control, and CIP spray performance all deserve review under partial-fill conditions.
Material and capacity decisions are linked
It is tempting to separate material choice from capacity planning, but in practice the two decisions interact. A larger tank makes surface condition, weld quality, and thermal design more important because sanitation failures and temperature deviations are harder to correct at scale. Likewise, the suitability of the material is partly tested by the cleaning regime required for the chosen capacity and product type.
For example, a small vessel with easy visual access may tolerate a less refined maintenance routine without immediate problems. Scale that same design up, and hidden residues around fittings or rough weld zones can become recurring contamination points. The vessel may still be structurally acceptable, yet operationally weaker than expected.
Spirit type and wash composition can shift the best answer
Whiskey, vodka, and brandy production do not always place the same demands on fermentation vessels. Grain-based washes may present different solids handling and cleaning challenges than fruit-based ferments. Some operations prioritize a clean, neutral profile; others accept or even seek more complex fermentation-derived character before distillation. Material and tank geometry should be judged in that process context.
A technical evaluator may therefore reach different conclusions for the same tank depending on whether the line runs relatively clear ferments, high-solids mashes, or recipes with frequent changeovers. The more variation in the plant schedule, the more valuable robust cleanability and controllable working volume become.
What buyers should check first in a technical review
Before comparing quotations in detail, it helps to screen a tank against the process realities that most often cause trouble after installation:
- Actual batch target: Is the required output based on nominal or working volume?
- Vessel geometry: What are the diameter-to-height implications for pressure, heat transfer, and cleaning?
- Cooling design: Is jacket coverage sufficient, and can utilities support peak fermentation heat?
- Interior finish: Are welds, corners, drains, and fittings designed for hygienic cleaning?
- Operating flexibility: Will the tank behave predictably at partial loads or with different mash characteristics?
- Maintenance burden: Are sensors, valves, gaskets, and manways accessible and easy to service?
Documentation review should also go beyond the vessel drawing. Buyers often need fabrication details, material traceability where relevant, finishing information, and clear confirmation of what accessories are included. The tank body may be acceptable while the practical weak points lie in valves, seals, sampling points, or poorly considered CIP arrangements.
Where evaluation errors usually occur
One common mistake is to compare capacity only by cost per liter. That approach can hide the fact that a lower-cost vessel may require more conservative fills, longer cleaning cycles, or tighter operator intervention to maintain fermentation stability. Another is to assume that stainless steel by itself guarantees hygienic performance. In real use, finish quality, geometry, and maintenance discipline decide whether the material advantage is actually realized.
Technical teams also sometimes underestimate the effect of utility limits. A fermenter can be correctly sized for production planning but mismatched to the site’s cooling water temperature, pump capacity, or ambient heat load. When that happens, fermentation control problems are blamed on yeast or process recipe when the real issue is vessel-utility integration.
The best purchase decisions usually come from matching vessel design to the full operating system: recipe, cycle time, cleaning regime, utilities, expected fill range, and sensory targets. Material and capacity are central to that decision, but they only deliver value when reviewed as part of the fermentation process rather than as standalone specifications.
For distilleries expanding capacity or replacing older vessels, the question is not whether bigger tanks or stainless construction are generally good choices. It is whether the specific tank design will keep fermentation stable under the plant’s actual conditions. That is the point where a vessel stops being a commodity and becomes process equipment.
Related News
- Hydrogen Storage Choices Get Costly at Utility ScaleApr 27, 2026Hydrogen storage drives utility-scale power costs in the energy transition. Explore hydrogen economy trade-offs across PEM electrolysis, cryogenic liquid hydrogen, transport, and decarbonization technology.
- Cryogenic Liquid Hydrogen Storage Has a Boil-Off ProblemApr 27, 2026Cryogenic liquid hydrogen and hydrogen storage face a major boil-off challenge shaping the hydrogen economy, hydrogen transport, and zero-carbon infrastructure—see practical insights for safer, scalable decarbonization.
- Vacuum insulated cryogenic vessels for liquefaction: managing boil-offSep 04, 2026Vacuum insulated cryogenic vessels for liquefaction help reduce hydrogen boil-off, manage pressure, protect product yield, and lower lifecycle costs. Explore key evaluation criteria.
- What ISO Standards Apply to Hydrogen Storage Tank Procurement?Sep 05, 2026What ISO standards apply to hydrogen storage tank procurement? Explore key requirements for gaseous, liquid, vehicle, and station storage to specify compliant systems.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Marcus Valve
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.