What does hydrogen pipeline compliance require for safe gas service?




A hydrogen line can appear ready for service after pressure testing, welding review, and document closeout, yet still fail the practical test of safe operation if its materials, joints, isolation points, or monitoring arrangements are not appropriate for hydrogen. The consequences are not limited to a failed inspection: a small leak can create an ignition hazard, unverified material performance can shorten asset life, and incomplete records can make later maintenance or incident investigation unreliable.
Hydrogen pipeline compliance requires a controlled, traceable demonstration that the piping system is designed, fabricated, examined, tested, operated, and maintained for hydrogen service. In practice, this means applying the governing code of record—often including ASME B31.12 where applicable—alongside local legal requirements, owner specifications, equipment standards, and documented risk controls. A successful hydrostatic or pneumatic test alone does not establish compliance. The full system must show pressure integrity, hydrogen-compatible materials, qualified joining, leak-tight assembly, controlled commissioning, and a workable inspection and management process.
Start with the correct compliance boundary
The first failure point is often administrative rather than mechanical. A project may refer generally to “hydrogen-ready” piping without defining whether the line carries pure hydrogen, a hydrogen-natural-gas blend, hydrogen at elevated pressure, or a process stream containing hydrogen with other gases. These are not interchangeable service descriptions. Gas composition, pressure, temperature, cycling frequency, location, and consequence of release affect the design basis.
Before reviewing fabrication records or inspection reports, establish the compliance boundary in writing. It should identify:
- the fluid composition, expected purity, contaminants, and whether composition can vary during operation;
- normal, upset, design, and test pressures and temperatures;
- the pipeline category and physical limits, including tie-ins, vents, drains, stations, valves, and connected equipment;
- the governing jurisdiction, code of record, owner requirements, and applicable editions or approved deviations;
- the intended operating mode, particularly pressure cycling, intermittent operation, and start-stop service;
- the hazardous-area classification and interfaces with detection, ventilation, electrical equipment, and emergency shutdown systems.
This definition prevents a common gap: components are individually purchased to acceptable specifications, but the assembled system has never been evaluated as a hydrogen service system. Compliance should follow the actual service envelope, not the broadest label in a procurement description.
Material compatibility is more than checking the material grade
Hydrogen can reduce ductility and fracture resistance in susceptible metallic materials under certain combinations of stress, microstructure, pressure, temperature, and hydrogen exposure. The relevant concern is often described as hydrogen-assisted cracking or hydrogen embrittlement, but the compliance task is broader: determine whether every pressure-retaining material is suitable for its intended duty.
A material certificate confirms what was supplied. It does not automatically prove that the item is acceptable for the actual hydrogen environment. Review should connect the material specification to design conditions and fabrication history. Carbon and low-alloy steels, stainless steels, weld metals, bolting, valve trim, seals, and small-bore fittings may each have different limitations. Hardness, strength level, heat treatment, welding process, and residual stress can influence performance.
Material verification therefore needs a disciplined chain of evidence. Confirm material identification and traceability from receiving through installation. Check that pipe, fittings, flanges, valves, and branch connections match approved material specifications. Review weld procedure qualifications and filler-metal selection for the required service. Where hardness restrictions, post-weld heat treatment, or specific toughness requirements apply, verify that records demonstrate compliance rather than assuming the purchase specification covers them.
Nonmetallic materials deserve equal attention. Seals, gaskets, valve seats, packing, hoses, coatings, and thread compounds can experience permeation, swelling, extraction of additives, loss of elasticity, or degradation. A gasket that performs well in another gas service may not retain the required leak-tightness after repeated hydrogen pressure and temperature cycles. The evaluation should cover the exact material, pressure range, temperature range, and installation configuration, including whether a seal is static, dynamic, exposed to vibration, or frequently decompressed.
Design review must address hydrogen-specific release paths
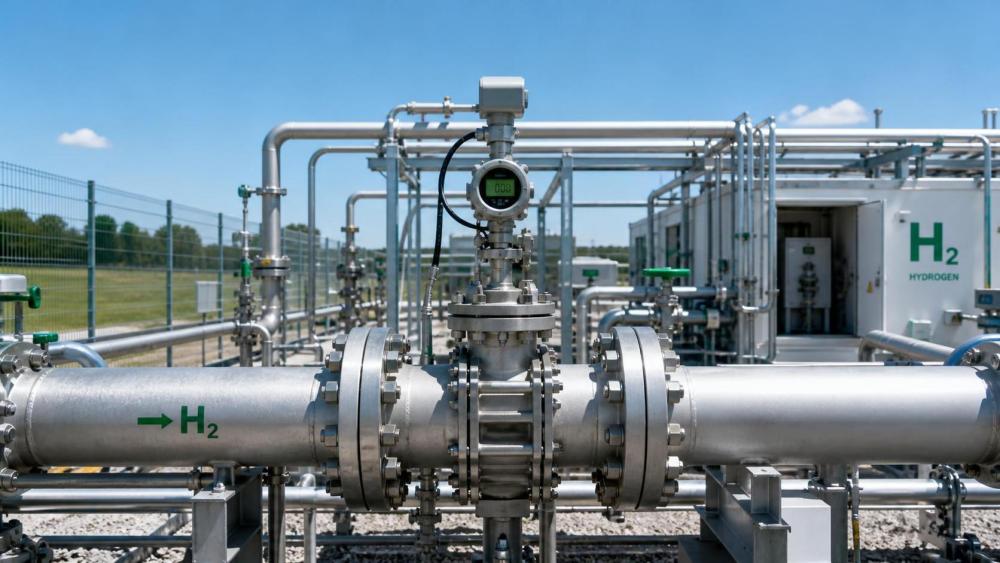
Hydrogen’s small molecular size and low ignition energy make leak control central to hydrogen pipeline compliance. The design review should look beyond the pipe wall and examine every location where gas can escape: flanged joints, threaded connections, valve stems, instrument connections, compression fittings, vents, drains, sample points, temporary connections, and interfaces between piping classes.
Threaded joints are a recurring source of concern in high-pressure or critical gas service. Whether they are permitted depends on the code of record and project requirements, but their presence should trigger a documented review of location, pressure, accessibility, vibration exposure, sealing method, and inspection approach. Similarly, dead legs, poorly arranged vents, unprotected low points, and inaccessible fittings can complicate purging and leak testing.
Pressure design must also account for credible transient conditions. Compressor trips, rapid isolation, thermal expansion of blocked-in sections, relief scenarios, and repeated pressurization cycles can govern loads that are not obvious from normal operating pressure alone. Pipe supports, anchors, flexibility, vibration restraint, and nozzle loads should be assessed as part of the system, particularly near compressors, control valves, and skid interfaces.
Do not treat relief and vent systems as secondary details
A pressure relief device is only effective when its discharge route is safe. Compliance review should verify the relief basis, set pressure, capacity assumptions, discharge piping, supports, backpressure effects, termination location, and separation from ignition sources or occupied areas. Vent lines need the same attention. They must be routed to a location where released hydrogen can disperse safely, with appropriate consideration of elevation, enclosure geometry, nearby air intakes, and potential accumulation zones.
Emergency isolation also needs a realistic operating philosophy. Identify which valves must close during a detected leak, fire, loss of utility, or abnormal pressure condition; determine whether fail-safe action is suitable; and confirm that shutdown does not trap gas in a section exposed to heat or leave an unsafe pressure differential across equipment.
Fabrication records should prove control, not merely completion
Field installation can introduce risks that are absent from a clean design package. Misidentified spools, unauthorized substitutions, inadequate joint preparation, uncontrolled repairs, incorrect gasket installation, and undocumented rework can all weaken the compliance case. The document package should allow an independent reviewer to trace each critical element from approved design through final acceptance.
For welded piping, the review normally includes approved welding procedures, welder qualifications, weld maps, consumable control where required, fit-up records, preheat or post-weld heat treatment records when applicable, and the specified nondestructive examination results. Acceptance criteria must match the governing construction code and approved project requirements. It is not enough that an examination was performed; the extent, method, examiner qualification, report identification, and disposition of indications should be clear.
Mechanical joints require similar discipline. Verify flange facing condition, gasket type and size, bolt material, lubrication assumptions, tightening method, and recorded bolt-load or torque controls where specified. In hydrogen service, inconsistent bolting practices can become a leak problem after temperature changes or pressure cycling. Valve orientation, flow direction, actuator settings, tag identification, and stroke testing should also be recorded before the system is enclosed or insulated.
Testing needs to establish strength, tightness, and safe readiness for gas introduction
Pressure testing is often viewed as the final gate, but it has several distinct purposes. A strength test evaluates structural integrity at the prescribed test condition. A leak test evaluates whether joints and components remain sufficiently tight. A commissioning leak check after introduction of the service gas or an approved surrogate may reveal issues not evident during earlier tests. The exact sequence, medium, pressure, hold period, acceptance criteria, and safety controls must follow the governing requirements and approved procedures.
Pneumatic testing deserves particular care because compressed gas stores substantial energy. A test plan should define exclusion zones, test boundaries, temporary restraints, calibrated gauges, pressure increments, communication methods, emergency actions, and formal authorization to proceed. Blind flanges, temporary hoses, manifolds, and test fittings must be rated and secured for the test condition. The risk review should not focus solely on permanent piping while overlooking temporary test equipment.
Prior to hydrogen introduction, systems commonly require cleaning, drying, purging, and verification that unwanted oxygen, moisture, construction debris, or incompatible gases have been reduced to the limits established by the operating procedure. The acceptable method depends on the system design and service requirements. Purging must be planned around vent routing, ignition control, gas detection, isolation, and avoidance of hazardous mixtures. Records should show the approved procedure, responsible personnel, measured parameters where required, and authorization for each transition.
Inspection after commissioning is part of compliance
A pipeline does not remain compliant simply because its initial turnover dossier was accepted. Hydrogen service can expose weaknesses gradually through pressure cycling, vibration, thermal movement, corrosion under insulation, seal aging, valve packing wear, or changes in gas quality. An integrity management approach should translate the original design assumptions into recurring field controls.
Useful inspection planning begins by ranking locations that are most likely to leak or degrade: compressor connections, vibrating small-bore branches, flanges subjected to thermal cycles, valve stems, instrument takeoffs, low-point drains, aboveground transitions, buried-to-aboveground interfaces, and areas where water ingress or external corrosion may occur. Inspection intervals should be based on the governing requirements, equipment condition, operating history, and risk assessment—not on convenience alone.
Management of change protects the original compliance case
Changes that appear minor can invalidate earlier assumptions. Replacing a valve with a different trim material, moving a detector, altering a relief discharge, changing the gas blend, increasing set pressure, or installing a new branch line may affect the system’s hazard profile. A management-of-change process should require technical review before implementation, not after an issue appears in the field.
The review should ask whether the change affects design pressure, materials, pressure relief, classified areas, electrical interfaces, supports, inspection requirements, operating procedures, or emergency response. It should also confirm whether drawings, line lists, hazardous-area documents, maintenance instructions, and training materials need revision. Closing a change request without updating the controlled records leaves operators relying on an obsolete system description.
Documents that should be available when the line is questioned
When an auditor, maintenance team, or incident investigator asks whether a section of line is fit for hydrogen service, the answer should not depend on memory. The essential evidence should be retrievable and internally consistent. This normally includes the design basis; piping and instrumentation diagrams; line lists; material specifications; isometric drawings; pressure calculations where required; component data; welding and examination records; pressure and leak-test reports; relief documentation; commissioning procedures; calibration records for relevant instruments; inspection history; and approved change records.
Hydrogen pipeline compliance is strongest when these documents reflect the installed condition rather than an earlier design intent. Redlined drawings that never become controlled as-built documents, missing material traceability at a repair location, or test packs that do not clearly identify system boundaries are warning signs. The corrective action is not simply to collect more paperwork. It is to reconcile physical configuration, operational limits, and records until each supports the same safety case.
Where service conditions are outside the assumptions of the selected code, involve the responsible engineering authority before operation or modification. The critical question is not whether a pipeline has a general approval label; it is whether its verified design, construction, testing, and ongoing controls are adequate for the hydrogen service it is actually expected to perform.
Related News
- Which logistics packaging best protects vacuum insulated piping in transit?Sep 03, 2026Logistics packaging for vacuum insulated piping: discover engineered transport frames, moisture barriers, and monitoring controls that reduce transit damage and protect cryogenic project schedules.
- What does hydrogen pipeline compliance require for safe gas service?Sep 02, 2026Hydrogen pipeline compliance: learn the essential requirements for safe gas service, from material compatibility and leak testing to commissioning and integrity management.
- How to Align Hydrogen Storage Contracts with ASME B31.12Sep 05, 2026How to align hydrogen storage contracts with ASME B31.12? Learn to define code boundaries, require traceability, set test gates, and reduce project risk.
- Pipeline Infrastructure Benchmarking: Which Throughput and Heat-Loss Metrics Matter Most for VIP Design?Aug 10, 2026Pipeline infrastructure benchmarking made practical: discover the throughput and heat-loss metrics that matter most for VIP design to improve cryogenic efficiency, flow stability, and smarter project decisions.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Marcus Valve
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.