
Are Alkaline Electrolyzers Better for Remote Hydrogen Production?




The remote-production question is really a system-design question
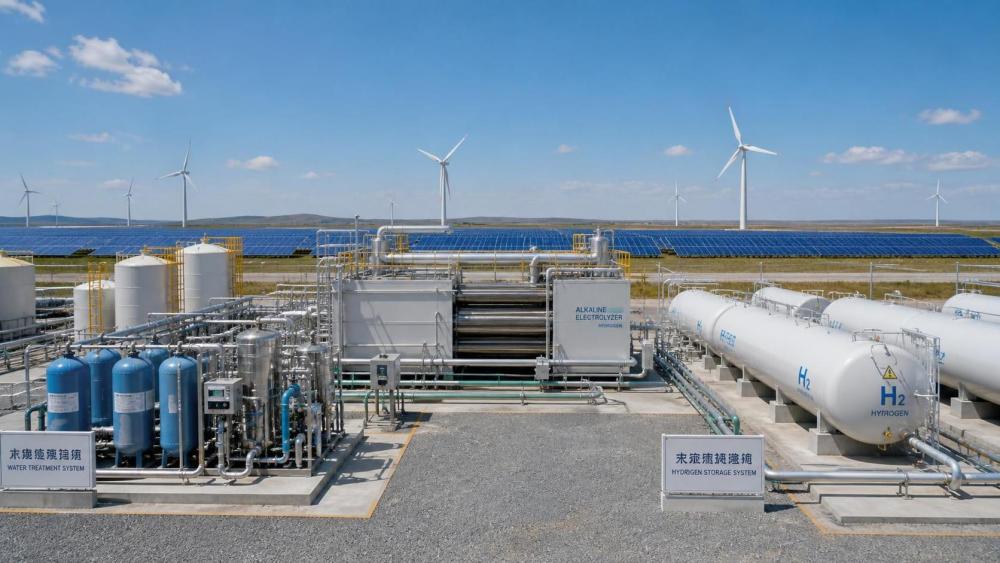
Remote hydrogen projects are often framed around a simple technology choice: alkaline electrolysis or PEM electrolysis. That framing is understandable, but incomplete. For a site far from industrial water supply, grid reinforcement, specialist maintenance teams, and established hydrogen offtakers, the electrolyzer is only one part of the decision.
The more useful question is whether an alkaline electrolyzer supports the operating model the project can realistically sustain. Can the site deliver reasonably stable electrical input? Can it secure and treat enough water? Can operators safely manage electrolyte, hydrogen compression, storage, and dispatch? Is the project designed to produce hydrogen continuously for a local anchor customer, or to absorb irregular surplus power from solar and wind assets?
Alkaline systems are often strong candidates for remote hydrogen production because they are mature, available at large capacities, and generally built around materials with a lower exposure to some scarce-metal supply chains than PEM systems. They have a long operating history in industrial hydrogen applications. Yet remote deployment changes the weighting of familiar advantages. A lower stack cost can be overshadowed by water handling, logistics, low utilization, service access, or the need to operate safely under highly variable renewable generation.
For energy developers, utilities, mining operators, industrial firms, and public-sector infrastructure planners, the answer is therefore conditional: alkaline electrolysis can be better for remote production when the project is built around steady operation and local operational discipline. It is less compelling when flexibility, compactness, rapid response, or constrained water and power conditions dominate the investment case.
Where alkaline electrolysis has a credible advantage
Alkaline electrolyzers use an aqueous alkaline electrolyte, commonly potassium hydroxide, to separate water into hydrogen and oxygen. The technology is well understood, with a broad installed base and a supply chain that has expanded rapidly alongside global hydrogen-policy ambitions. In the right setting, this maturity matters more than it may appear in a technology comparison.
A remote project with a stable power profile is the most natural fit. This could include a hydro-powered site, a geothermal resource, a wind-and-solar project supported by sufficient battery storage, or a facility connected to a relatively reliable local grid. Where the electrolyzer can run for long periods near its design point, alkaline equipment can translate its established operating characteristics into predictable hydrogen output.
That predictability has practical value. Hydrogen transport is expensive and operationally demanding, whether the product is compressed, liquefied, converted into ammonia or another derivative, or consumed directly at the site. A mine using hydrogen for haulage, a remote industrial hub replacing diesel, or an isolated power system using hydrogen for long-duration storage needs a production asset that matches its downstream demand. A system that operates steadily is often easier to integrate with compression, storage, and distribution equipment than one that repeatedly swings between very low and very high output.
Alkaline technology can also appeal where project sponsors are trying to avoid a narrow dependence on critical material markets. PEM electrolyzers typically rely on platinum-group metals and titanium-intensive components, although material loading and supply strategies continue to improve. Alkaline systems are not free of supply-chain or manufacturing constraints, but their conventional material base can be strategically attractive for governments and operators considering local manufacturing, long-term replacement parts, and geopolitical resilience.
For large projects, scale matters as well. The central question is not simply the nameplate rating of an electrolyzer package. It is whether a supplier can deliver an integrated system with power electronics, water treatment, gas purification, controls, safety systems, spares, commissioning support, and long-term service. Alkaline suppliers with demonstrated industrial references may offer a more familiar delivery path for projects whose principal risk is execution rather than laboratory-level performance.
Why “lower cost” is an unreliable shortcut
A common claim is that alkaline electrolysis is automatically the lower-cost option. It may be less expensive on selected capital-cost measures, but remote hydrogen economics cannot be judged from stack pricing or a headline cost per kilowatt alone. The delivered cost of hydrogen depends on the complete system: renewable power, interconnection or microgrid equipment, water sourcing and treatment, civil works, compression, storage, transport, operations, insurance, financing, and the utilization rate of each asset.
Low utilization is especially damaging. A remote solar site may have excellent annual irradiation yet provide a strongly variable daily power profile. A wind site may have high annual energy yield but extended calm periods. If the electrolyzer, compressor, storage vessels, and site team are sized for peak renewable output but operate only intermittently, fixed costs are spread over fewer kilograms of hydrogen.
In this situation, the apparent equipment saving of an alkaline system may not decide the project. Developers should model at least several operating cases: direct coupling to renewable output, operation with battery buffering, operation with a grid or generator back-up source, and curtailed-power operation. The useful comparison is the annual hydrogen delivered at the required pressure and purity, not merely the annual electrical energy sent to the electrolyzer.
Power quality and plant operating limits deserve the same attention. Modern alkaline electrolyzers can manage load changes better than earlier generations, but specific ramping behavior, minimum-load thresholds, gas crossover management, pressure balance, and restart procedures vary by supplier and configuration. A generic statement that alkaline systems “cannot follow renewables” is outdated. The equally broad claim that they handle intermittency with no operational penalty is also unsafe. The relevant question is how a particular system performs under the project’s actual hourly power profile.
Water is often the first remote-site constraint
Hydrogen is frequently discussed as though electricity were the only essential input. At a remote site, water can be the gating factor. Electrolysis consumes water directly, but the practical requirement is higher than the theoretical reaction demand because treatment, cooling, blowdown, purification, and maintenance all create additional demand. The exact balance depends on plant design and local conditions and should be verified with the selected supplier.
Alkaline systems generally require appropriately purified water and careful chemistry control. This does not mean they are unsuitable for arid regions or coastal locations. It means the water strategy has to be developed as a core plant package, not left as a utility detail.
- For inland sites, assess seasonal water availability, water rights, competing community and agricultural demand, and the quality of the raw source.
- For coastal sites, assess desalination capacity, intake and discharge permits, corrosion management, and the power required for water treatment.
- For sites using recycled industrial water, validate contaminants, treatment reliability, and operational responsibility before treating the source as bankable.
- For all locations, plan for water storage, sampling, monitoring, consumables, and upset conditions rather than assuming continuous access to specification-grade feedwater.
Remote operations add another layer: alkaline electrolyte management. Potassium hydroxide is a routine industrial chemical, but it is corrosive and requires disciplined storage, transfer, containment, personal protective equipment, and emergency response. At a staffed industrial site with established chemical-handling systems, this may be manageable. At an unmanned or lightly staffed renewable-energy outpost, it can materially affect the design of the operations model.
PEM systems also demand high-purity water and are not exempt from water-risk planning. Still, where site footprint, simplicity of balance-of-plant, or fast deployment is the priority, developers should examine whether the alkaline electrolyte loop introduces an operational burden that outweighs its other benefits.
Match the technology to the hydrogen use case
Remote hydrogen production is not one market. The right technology changes with the form in which hydrogen will be used, the required delivery pressure, and the tolerance for variable output.
Consider a remote ammonia project with access to renewable power that is diversified across wind, solar, storage, and perhaps a firm generation source. Its downstream synthesis loop benefits from a stable hydrogen supply. Here, alkaline electrolysis can be a logical choice, particularly when plant scale is substantial and the project can support a professional operating team. The key challenge may be synchronizing hydrogen production with ammonia synthesis, nitrogen supply, storage, port logistics, and export commitments.
Now consider a network of remote vehicle refueling stations. Demand may be uneven, hydrogen storage space limited, and dispensing requirements may involve pressures of 70 MPa or above. The site may need frequent load changes and compact integration with compression and pre-cooling equipment. Alkaline electrolysis can still be considered, but PEM may have an advantage where dynamic behavior and footprint are more valuable than equipment cost. Compliance with hydrogen-refueling requirements, including relevant frameworks such as ISO 19880 and SAE J2601 where applicable, cannot be deferred until after the electrolyzer selection.
A third case is a mining operation seeking to displace diesel in haul trucks, power generation, or process heat. This is often presented as an ideal remote-hydrogen use case because diesel logistics are costly and emissions reduction has strategic value. In reality, the demand profile is decisive. A mine with round-the-clock demand, stable renewable generation, and a capable maintenance workforce may favor alkaline equipment. A mine with highly variable load, aggressive production schedules, limited water, and no appetite for chemical-process operations may assign greater value to PEM flexibility or may determine that a hybrid supply strategy is necessary.
Safety and serviceability cannot be treated as secondary packages
Every remote hydrogen project faces the same basic reality: hydrogen is difficult to contain, easy to ignite across a wide concentration range, and often handled at pressures that amplify the consequences of design or operating failures. The electrolyzer technology does not remove this risk. It changes the operational interfaces that must be controlled.
Project teams should review the full hydrogen pathway, from water intake to final use. That includes electrical isolation, hydrogen and oxygen separation, venting, detection, hazardous-area classification, pressure relief, emergency shutdown logic, compressor protection, storage spacing, grounding, and communications during power or network loss. The design basis should reference the jurisdiction’s applicable codes and standards. For pipeline and distribution components, ASME B31.12 may be relevant; for refueling infrastructure, ISO 19880 and related national rules may apply. The exact legal and certification pathway should be confirmed locally rather than assumed from an international standard list.
Remote locations create a serviceability issue that is sometimes underestimated during procurement. A vendor’s performance guarantee has limited practical value if technicians, replacement parts, calibration equipment, or electrolyte-management expertise take weeks to reach the site. Buyers should ask for a site-specific service plan, including remote diagnostics, response commitments, critical-spares inventory, training requirements, stack replacement assumptions, and responsibility for software support over the intended asset life.
It is also worth distinguishing between a technically operating plant and an operationally resilient one. A resilient plant can safely degrade, shut down, restart, and continue functioning when communications fail, renewable production drops, a water-treatment skid trips, or a compressor is unavailable. These scenarios should be tested in front-end engineering, not discovered after commissioning.
A practical selection process
The most effective procurement process starts with the operating envelope rather than a preferred technology. Before requesting quotations, define an hourly or sub-hourly power profile, hydrogen demand profile, delivery pressure, purity requirement, water source, site access constraints, climate conditions, staffing model, and planned expansion path. Those inputs allow suppliers to show how their equipment behaves in a real project instead of presenting an optimized brochure case.
Then evaluate alkaline and PEM options against a consistent set of questions:
- What annual operating hours and load distribution does the equipment need to achieve the stated efficiency, availability, and degradation assumptions?
- What are the minimum stable load, ramping limits, restart sequence, and expected maintenance implications under the proposed renewable profile?
- What water quality is required at the electrolyzer boundary, and what treatment plant, chemicals, consumables, and operator attention are assumed?
- What hydrogen purity, pressure, drying, purification, compression, and storage equipment are included in the proposed scope?
- Which safety systems, certifications, and local regulatory approvals are included, and which remain the owner’s responsibility?
- What site data, reference installations, warranty terms, spare-parts strategy, and long-term service capabilities substantiate the promised performance?
Financial models should stress-test the assumptions that matter most. Test lower renewable availability, higher water-treatment cost, delayed permitting, reduced hydrogen demand, and longer maintenance outages. In remote projects, downside cases are often driven by logistics and utilization rather than by a small difference in electrolyzer efficiency.
What to watch as remote hydrogen moves from concept to infrastructure
The market is moving beyond the stage where electrolyzer capacity announcements alone define project quality. Governments and investors increasingly need evidence that projects can connect low-carbon power, water, permits, offtake, transport, and safety systems into an investable whole. This favors developers who treat technology selection as part of infrastructure planning rather than a stand-alone equipment purchase.
Alkaline electrolysis is likely to remain important in that transition. Its established industrial foundation, potential fit with steady power, and relevance to large-scale hydrogen production make it a serious option for remote sites. But it is not a default answer for every off-grid application.
For remote hydrogen production, alkaline systems are best understood as a strong tool for a defined operating environment: stable enough electricity, manageable water and chemical logistics, sufficient site capability, and a hydrogen demand profile that rewards sustained production. Where the project instead depends on rapid response to variable power, compact deployment, or lightly staffed operations, the comparison should remain open. The decision should follow the site’s constraints, because those constraints will ultimately determine whether hydrogen becomes usable infrastructure or an expensive stranded asset.
Related News
- Are Alkaline Electrolyzers Better for Remote Hydrogen Production?Sep 02, 2026Are alkaline electrolyzers better for remote hydrogen production? Explore costs, water needs, flexibility, safety, and the best fit for your site.
- How to Schedule Annual Maintenance for an Alkaline ElectrolyzerSep 01, 2026How to schedule annual maintenance for alkaline water electrolysis? Learn how to plan a safe, data-driven outage, secure critical spares, protect stack life, and ensure reliable hydrogen production.
- Is sovereign hydrogen infrastructure investment worth the long payback?Aug 15, 2026Sovereign hydrogen infrastructure investment can pay off despite long payback periods when it strengthens energy security, unlocks demand, and creates durable industrial advantage. Explore the strategic case.
- What Determines Stack Efficiency and Lifetime in an ALK Electrolysis Plant?Aug 08, 2026ALK electrolysis plant performance depends on stack materials, separator stability, electrolyte quality, temperature control, and load profile. Learn what truly drives efficiency, lifetime, and lower hydrogen cost.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.