How to Schedule Annual Maintenance for an Alkaline Electrolyzer




Knowing how to schedule annual maintenance for alkaline water electrolysis is less about picking a date on a calendar and more about planning a controlled outage around the actual condition of the plant. The annual service window should protect stack life, hydrogen purity, safety barriers, and production availability without turning routine work into an unnecessary overhaul.
For an alkaline electrolyzer, the best schedule combines the OEM maintenance manual, operating history, process trends, spare-part lead times, and site safety requirements. A unit that has operated steadily at moderate load does not necessarily need the same scope as one that has experienced frequent starts, water-quality excursions, unstable differential pressure, or declining production efficiency.
A practical rule is to begin planning the annual outage three to six months before the intended shutdown. That gives the operations team time to review data, secure qualified service support, order long-lead components, coordinate hydrogen isolation, and avoid a maintenance window that clashes with high-value power or hydrogen delivery commitments.
How to Schedule Annual Maintenance for Alkaline Water Electrolysis
Start with the manufacturer’s recommended interval and task list, then adjust the scope using evidence from your own asset. The OEM manual remains the governing document for stack handling, electrolyte concentration, torque procedures, pressure testing, calibration, and approved replacement parts. It should not be replaced by a generic checklist.
Next, look backward over the previous twelve months. Review production records, operating hours, start-stop cycles, stack voltage trends, cell-voltage spread where available, hydrogen and oxygen purity results, electrolyte sampling, water-treatment records, alarms, trips, leaks, and corrective maintenance. The aim is simple: identify whether the planned annual outage should remain routine or become a condition-based intervention.
A useful direct answer is this: schedule the annual maintenance shutdown after reviewing operating trends and before known risk indicators become failures; reserve enough time for safe isolation, inspection, testing, and restart verification; and order parts only after the final scope is agreed with the OEM or a qualified service provider.
Do not schedule the date first and force every task into it later. That approach often creates either a rushed shutdown or a prolonged outage caused by missing parts, incomplete permits, or discoveries that were predictable from operating data.
Choose the Maintenance Window Based on Risk, Not Just the Calendar
Many sites target an annual outage because it fits budgeting and workforce planning. That is reasonable, but the calendar alone is weak justification. An alkaline electrolyzer is a process system with electrical, chemical, mechanical, and gas-handling risks. The correct window depends on what the equipment has experienced.
Bring the outage forward when there are repeated purity alarms, unexplained increases in specific energy consumption, persistent electrolyte loss, recurring seal leaks, abnormal pump vibration, worsening cooling performance, inconsistent pressure control, or a rising number of nuisance trips. These signs do not automatically mean the stack has failed. They do mean that waiting for the planned annual date may turn a manageable inspection into an unplanned production loss.
Conversely, a unit with stable operating data may need a focused annual service rather than intrusive stack work. Opening a stack without a documented reason can introduce contamination, sealing errors, mechanical damage, and unnecessary downtime. “More maintenance” is not automatically better maintenance.
For plants supporting a firm hydrogen supply contract, build the annual plan around the commercial operating profile. Confirm whether stored hydrogen, parallel production assets, or alternative supply can cover the shutdown. Maintenance planners should also check whether the electrical supply, water-treatment system, compressor train, storage system, and downstream users have their own outage requirements. An electrolyzer outage is rarely isolated from the rest of the hydrogen facility.
Build the Scope From Operating Evidence
The annual work package should distinguish between mandatory OEM tasks, condition-driven inspections, and optional improvements. Combining all three into one undifferentiated list makes it difficult to control cost, duration, and responsibility.
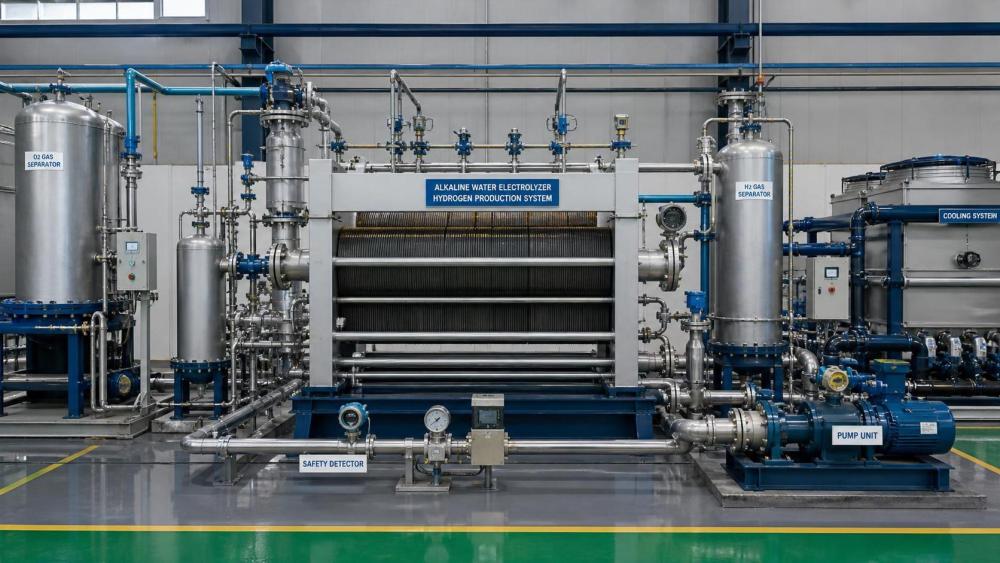
Mandatory tasks normally include functional checks of safety devices, instrumentation verification, inspection of accessible piping and connections, review of electrical enclosures and grounding, checks of pumps and valves, confirmation of cooling-system condition, examination of gas-liquid separation equipment, and inspection of ventilation and gas detection systems. Exact requirements vary by design and jurisdiction, so use the applicable site procedures and approved documentation.
Condition-driven work is where maintenance teams add value. For example, electrolyte sampling may show contamination or concentration drift that calls for controlled treatment or replacement. Water-treatment records may indicate cartridge exhaustion, resin degradation, or insufficient feedwater quality. Trending can reveal whether a pressure transmitter should be recalibrated, whether a pump seal is approaching failure, or whether a heat exchanger requires cleaning.
Stack-related work deserves particular discipline. A higher stack voltage can be associated with several causes, including normal ageing, temperature deviation, electrolyte condition, contact resistance, gas management issues, or operating changes. It is not proof that the stack should be opened. Compare the trend against comparable operating points and consult the OEM before committing to intrusive disassembly.
Items that are frequently missed
Small supporting systems often create the most disruptive outages. Review emergency shutdown logic, gas detectors, ventilation interlocks, drain systems, caustic-handling equipment, sample points, relief devices, instrument impulse lines, and cable terminations. Confirm that calibration certificates, inspection records, and drawings reflect the equipment actually installed.
Also check the condition and availability of consumables: approved gasket materials, filters, pump seals, valves, instrument spares, electrolyte-handling supplies, personal protective equipment, and emergency response materials. A shutdown can lose days over a low-cost item that was never placed on the materials list.
Prepare the Shutdown Before the Plant Stops
Good annual maintenance is mostly preparation. Freeze the scope early enough to complete engineering review, hazard assessment, permits, contractor onboarding, and materials inspection. Late additions should be controlled through a formal change process, particularly where they affect pressure boundaries, electrical systems, hydrogen service, or safety functions.
The shutdown plan should clearly define isolation boundaries. This includes electrical isolation, hydrogen and oxygen handling, depressurization, purging where required by the approved operating procedure, electrolyte draining or circulation arrangements, lockout-tagout, confined-space considerations, and verification of a safe work atmosphere. Alkaline electrolyte is caustic, while hydrogen and oxygen require careful management because of flammability and oxygen-enrichment hazards. These are not activities to improvise from a generic online checklist.
Assign one accountable outage coordinator and name the technical owner for each system. Operations, maintenance, process engineering, electrical personnel, safety staff, OEM representatives, and contractors should all work from the same controlled schedule. Daily coordination meetings are useful during the outage, but they should focus on unresolved technical issues, permit status, test results, and critical-path work rather than broad status reporting.
A simple schedule normally includes five phases:
- Pre-outage review: analyze data, agree the scope, confirm standards and permits, and order materials.
- Safe shutdown and isolation: place the unit in the approved condition for maintenance and verify energy isolation.
- Inspection and corrective work: complete planned checks, record findings, and manage deviations.
- Testing and reassembly: perform required pressure, leak, electrical, control, and safety-function checks.
- Controlled restart: verify stable operation before returning the plant to normal service.
Use the Outage to Verify Safety and Asset Integrity
An annual shutdown is one of the few times when a plant can test safeguards without production pressure driving shortcuts. Confirm the functionality of gas detection, ventilation, emergency shutdowns, alarms, interlocks, relief arrangements, and shutdown sequences according to the approved design basis and local requirements.
Inspection of pressure-containing equipment and hydrogen piping should be planned with the relevant jurisdictional rules, design documentation, and qualified inspection personnel. Reference standards can help frame the discussion, but a standard name is not a substitute for a site-specific compliance review. For example, ISO, ASME, and other recognized frameworks may apply differently depending on the system boundary, country, insurer, and authority having jurisdiction.
Material compatibility also deserves attention. Electrolyte exposure, temperature cycling, vibration, and gas service can affect seals, coatings, valves, and piping components over time. Replace components using materials approved for the exact service. A part that fits physically may be unsuitable for caustic electrolyte, oxygen service, hydrogen service, or the expected pressure and temperature range.
Do Not Treat Restart as a Formality
A maintenance outage is not complete when the last cover is fitted. Restart is a commissioning activity, especially after work on the stack, process piping, instrumentation, control logic, pressure boundaries, or safety systems.
Use a written return-to-service checklist. Confirm that all tools and temporary blinds have been removed, isolation points have been restored under authorization, instruments are calibrated, maintenance records are complete, leak and pressure tests have passed, and control-system changes have been reviewed. Then bring the electrolyzer online gradually in line with the OEM procedure.
During the first operating period, monitor the parameters most likely to reveal a problem: cell or stack voltage, temperature, pressure, differential pressure, electrolyte level and concentration, gas purity, cooling performance, water quality, pump behavior, and alarm frequency. Compare these values with pre-outage data at similar operating conditions. A clean restart is encouraging, but stable performance over the following days provides the more meaningful confirmation.
Capture Findings for Next Year’s Plan
The most useful annual maintenance report is not a list of completed tasks. It explains what was found, what was changed, why the decision was made, what test evidence supports return to service, and what should be monitored next. Photographing accessible degradation, recording part numbers and batch information, and documenting torque, calibration, and test records can prevent costly uncertainty later.
Classify findings into immediate corrective actions, items to monitor, and future capital or reliability work. For example, a recurring issue with water quality may point to an upstream treatment problem rather than an electrolyzer defect. Repeated process trips may require control tuning, instrument investigation, or operating-procedure changes. The annual outage should improve the reliability strategy, not merely restore the prior condition.
For large or strategically important hydrogen projects, technical benchmarking repositories such as G-HEI can be useful when teams need to compare maintenance governance, material-integrity considerations, and international reference frameworks across electrolysis and connected hydrogen infrastructure. The practical decision still belongs to the asset owner, OEM, and qualified site team working from the plant’s actual design and operating record.
Common Scheduling Mistakes
The first mistake is assuming the stack is the only component that matters. Pumps, water treatment, cooling, instrumentation, separators, electrical equipment, and safety systems can each limit availability.
The second is ordering spare parts after the shutdown begins. Long-lead components and OEM-approved stack materials need early confirmation. The third is combining too many improvement projects with essential maintenance. Separate mandatory reliability work from optional upgrades, then protect the critical path.
Another common error is failing to reserve time for troubleshooting and restart. A schedule that allows exactly enough time for ideal work execution has no realistic contingency. Include a controlled allowance for inspection findings and commissioning checks, particularly for assets with a history of leaks, purity issues, or unstable operation.
FAQ
Should an alkaline electrolyzer always be shut down exactly once per year?
Not necessarily. The OEM interval, regulatory obligations, duty cycle, and equipment condition govern the plan. Annual scheduling is common, but abnormal operating trends may justify earlier intervention.
Can maintenance be planned only from operating hours?
No. Operating hours matter, but start-stop cycles, load variation, water quality, electrolyte condition, alarms, and environmental conditions can be equally relevant.
Should the electrolyte always be replaced during annual maintenance?
Only when the OEM guidance and sample results support it. Replacement without a defined need can add cost, handling risk, and unnecessary waste-management work.
Who should approve a stack inspection?
The decision should involve the asset owner’s technical authority and the OEM or an appropriately qualified service provider. Stack disassembly requires controlled procedures and design-specific knowledge.
When deciding how to schedule annual maintenance for alkaline water electrolysis, treat the outage as a planned reliability event: use operating evidence to set the scope, prepare isolations and parts before shutdown, verify safety systems and asset integrity, and document the restart with the same care used for the maintenance work itself.
Related News
- Are Alkaline Electrolyzers Better for Remote Hydrogen Production?Sep 02, 2026Are alkaline electrolyzers better for remote hydrogen production? Explore costs, water needs, flexibility, safety, and the best fit for your site.
- How to Schedule Annual Maintenance for an Alkaline ElectrolyzerSep 01, 2026How to schedule annual maintenance for alkaline water electrolysis? Learn how to plan a safe, data-driven outage, secure critical spares, protect stack life, and ensure reliable hydrogen production.
- Is sovereign hydrogen infrastructure investment worth the long payback?Aug 15, 2026Sovereign hydrogen infrastructure investment can pay off despite long payback periods when it strengthens energy security, unlocks demand, and creates durable industrial advantage. Explore the strategic case.
- What Determines Stack Efficiency and Lifetime in an ALK Electrolysis Plant?Aug 08, 2026ALK electrolysis plant performance depends on stack materials, separator stability, electrolyte quality, temperature control, and load profile. Learn what truly drives efficiency, lifetime, and lower hydrogen cost.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.