
How to Verify a Supplier’s PEM Electrolyzer Delivery Capability




For utility-scale hydrogen projects, a supplier’s delivery capability is not proven by a nameplate capacity claim, a prototype stack, or a well-managed factory visit. PEM electrolyzer procurement involves a chain of interdependent commitments: stack production, titanium component sourcing, membrane-electrode assembly availability, power-electronics integration, testing capacity, export documentation, site commissioning, and warranty support. A weakness in any one of these areas can delay the entire project.
The practical question is therefore not whether a supplier can build a PEM electrolyzer. It is whether it can deliver the contracted system configuration, performance level, documentation package, and commissioning support within the required schedule—repeatedly, under the commercial and regulatory conditions of the destination market.
Verifying this capability requires evidence. The following approach separates credible industrial capacity from claims based mainly on pilot-scale experience.
Start by defining what “delivery” means in the contract
Delivery is often discussed too narrowly as shipment of skids or containers. For a hydrogen project, the usable delivery milestone may instead be factory acceptance, arrival at site, mechanical completion, successful commissioning, or performance acceptance under specified operating conditions. These are very different obligations.
Before evaluating any supplier, establish a delivery matrix that identifies:
- electrolyzer system capacity, number of trains, and phased expansion requirements;
- guaranteed hydrogen output, purity, pressure, specific energy consumption, availability, and turndown range;
- scope boundaries for rectifiers, deionized-water treatment, gas purification, cooling, controls, compression interfaces, and vent systems;
- factory acceptance test (FAT), site acceptance test (SAT), and performance-test conditions;
- shipping terms, preservation requirements, customs documentation, and local certification responsibilities;
- commissioning personnel, spares, remote monitoring, training, response times, and warranty remedies.
Without this definition, a supplier may appear to have delivered “a 20 MW project” when its actual responsibility ended at supplying stacks, while the customer or EPC contractor carried the integration, certification, and commissioning risk.
For large projects, ask suppliers to distinguish clearly between equipment manufacturing lead time and project delivery lead time. The former may look short because stack assembly is relatively fast once materials are available. The latter includes engineering freeze, long-lead procurement, package integration, FAT, transport, site readiness, energization, and the resolution of control-system or balance-of-plant issues.
Examine the stack manufacturing bottleneck, not only factory floor area
PEM electrolyzer capacity is frequently expressed in gigawatts per year. This number has limited value unless the supplier explains how it is calculated. A facility may have sufficient assembly space to claim a high annual output while lacking enough qualified production tools, trained operators, test stations, or material supply to sustain that output.
Ask for the current, demonstrated, and planned capacities separately:
- Current demonstrated capacity: equipment that has been commissioned, operated, and used for commercial production.
- Installed capacity: production capability based on equipment already in place, including operating shifts and realistic yield assumptions.
- Planned capacity: future expansion dependent on financing, equipment installation, qualification, or additional labor.
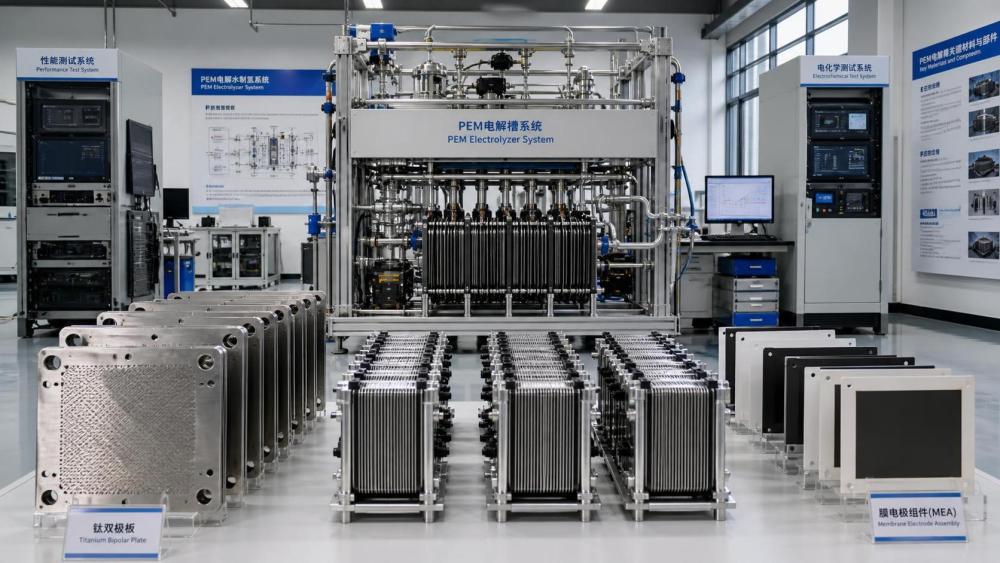
Then request a line-level explanation. The critical steps normally include catalyst-coated membrane preparation or procurement, membrane-electrode assembly production, porous transport layer handling, titanium bipolar plate fabrication or sourcing, stack compression and assembly, electrical testing, leak testing, and end-of-line performance validation.
A supplier that cannot show throughput by process stage may be masking a bottleneck. For example, an automated assembly line does not solve constraints in titanium machining, coating quality, membrane supply, curing cycles, or stack test duration. Similarly, a stated annual capacity should be challenged if it assumes continuous operation without allowance for commissioning downtime, rework, engineering changes, preventive maintenance, or customer-specific configurations.
Useful evidence includes production routing, key equipment lists, shift patterns, monthly output history, yield and rework data, and a rolling order book. Confidential figures can be reviewed under a non-disclosure agreement, but the underlying logic should remain auditable.
Trace the titanium supply chain to the actual component level
Titanium is one of the most consequential supply-chain exposures in PEM electrolysis. It is used in components that must resist corrosion in an acidic electrochemical environment while maintaining conductivity, dimensional stability, and gas-management performance. In many designs, titanium is required for bipolar plates and porous transport layers; coating systems may also be critical to long-term performance.
A supplier’s assurance that it has “strategic partners” is not enough. Verification should cover the specific grade, form, manufacturing route, coating process, qualification status, and geographic source of the titanium-containing parts used in the offered stack.
Questions worth asking include:
- Which components are titanium-based, and what is the annual consumption per MW of the proposed design?
- How many qualified sources exist for each critical component?
- Are suppliers approved at the raw-material, semi-finished, and finished-component levels?
- What incoming inspection, traceability, and lot-release controls are applied?
- Are key plate-forming, coating, or porous-material operations performed internally or by subcontractors?
- What buffer stock is held, and how is it allocated among committed projects?
Dual sourcing is valuable only when the second source has completed technical qualification and can meet the same performance requirements. A nominal alternative supplier that has not passed durability validation, corrosion testing, or dimensional repeatability checks does not materially reduce schedule risk.
The same discipline applies to membranes, iridium-containing catalysts, seals, power semiconductors, high-pressure valves, sensors, and control hardware. PEM supply chains are not constrained by a single material alone; delivery failures often emerge where an apparently standard component is tied to a specialized approved vendor or a long qualification cycle.
Review the order book and capacity allocation rules
Manufacturing capability has little meaning if most capacity is already committed. A supplier may be technically credible and still be unable to reserve the required production slots. This is especially important where several large projects are scheduled within the same 12- to 24-month period.
Request a capacity allocation view covering the period from engineering release to expected shipment. It does not need to disclose customer names, but it should show committed output, provisional reservations, internal buffer, and the capacity assigned to the proposed project.
Look for the commercial mechanism behind the allocation. Is capacity reserved only after advance payment? Does the supplier have the contractual right to move slots when upstream materials are delayed? Are project milestones linked to customer approvals that could cause the slot to be lost? What happens if a project is postponed after long-lead materials have been ordered?
The most reliable suppliers will connect the production reservation to a realistic master schedule and identify the dependencies that remain outside their direct control. A schedule that contains no procurement contingency, design-freeze date, logistics allowance, or FAT queue is more likely to be a sales schedule than an execution schedule.
Audit quality systems through records, not certificates alone
Quality certification is necessary but not sufficient. ISO 9001 certification demonstrates a quality-management framework; it does not independently prove that a particular PEM stack will meet performance and durability requirements at scale. The stronger question is whether the supplier can maintain traceability and process discipline when output rises.
During a factory audit, follow one completed stack or system package backwards through its records. The traceability file should link serial numbers to membrane and catalyst lots, titanium component batches, seals, assembly parameters, torque or compression records where relevant, leak-test results, electrical test results, non-conformance reports, rework history, and final release approval.
Pay attention to how deviations are handled. Every manufacturer has non-conformities. The important issue is whether deviations are identified early, contained, investigated, and closed through a documented corrective-action process. Repeated rework on the same component family, unusually broad acceptance limits, or incomplete material traceability are warning signs, particularly before a supplier scales production.
For packaged systems, inspect quality control beyond the stack. PEM electrolyzers are integrated plants. Pipe cleanliness, weld procedures, pressure testing, cable termination, instrument calibration, software version control, hazardous-area design, ventilation provisions, and emergency shutdown logic all influence site performance and safety.
Demand representative testing and understand its limits
A successful FAT should demonstrate more than basic start-up. The test protocol must reflect the contractual design and the actual project duty cycle. Verify that the test unit uses the same stack generation, controls architecture, rectifier configuration, materials, and major balance-of-plant equipment intended for delivery.
At a minimum, the test plan should define:
- hydrogen production rate and measurement method;
- hydrogen purity requirements and analytical instruments used;
- electrical consumption boundary and accuracy of power measurement;
- operating pressure, water quality, temperature, and ambient conditions;
- load range, start-stop behavior, ramping profile, and alarm response;
- leak-test and pressure-test requirements;
- acceptance criteria, repeat-test rules, and treatment of deviations.
Specific energy consumption figures require careful interpretation. A published number may refer only to the stack, exclude auxiliary loads, be measured at nominal rather than partial load, or use a different hydrogen-output basis. Compare suppliers using one agreed boundary: for example, electrical energy at the electrolyzer package inlet and hydrogen output at the defined battery limit. The contract should specify whether values are based on lower heating value or higher heating value where relevant.
Durability evidence needs equal scrutiny. Short demonstrations cannot establish multi-year stack behavior. Ask for operating-hour data from comparable stack designs, degradation trends, failure modes observed, maintenance interventions, and the relationship between the reference operating profile and the intended project profile. Dynamic operation linked to variable renewable power may create different stresses from steady baseload operation.
Validate references by similarity, recency, and scope
Reference projects are among the strongest indicators of delivery capability, but only if they are comparable. A supplier with numerous small demonstration units has not automatically demonstrated the ability to execute a multi-MW industrial facility. Conversely, a company may have delivered large systems but with a different stack platform, different pressure rating, or an EPC partner that carried most of the interface risk.
Reference checks should establish:
- the supplier’s precise scope of supply;
- commercial operation date versus shipment date;
- installed and operating capacity;
- actual availability, major outages, and root causes;
- commissioning duration and unresolved punch-list items;
- stack replacements, warranty claims, and response performance;
- similarity of operating profile, climate, water source, pressure, and regulatory setting.
Speak, where possible, with the asset owner or plant operator rather than relying only on a supplier-arranged presentation. Ask what surprised them during construction and commissioning. The answer often reveals more than the reference’s headline capacity.
Check standards compliance at the system boundary
International standards should be treated as design and evidence requirements, not as labels. Depending on the project location and scope, relevant frameworks may include ISO 22734 for hydrogen generators using water electrolysis, ISO 19880 series requirements for hydrogen fuelling infrastructure where applicable, ASME B31.12 for hydrogen piping, and local electrical, pressure-equipment, machinery, hazardous-area, and building regulations.
The applicable route will differ by jurisdiction. In the European Economic Area, equipment may need to satisfy legislation governing pressure equipment, machinery, electrical equipment, electromagnetic compatibility, and potentially explosive atmospheres. In North America and other markets, requirements may be shaped by local authorities having jurisdiction, recognized testing laboratories, and project-specific codes.
Do not accept a generic declaration of compliance. Require a compliance matrix identifying each applicable regulation or standard, the responsible party, evidence to be supplied, open items, and the point at which third-party inspection or certification is required. This is particularly important where equipment is assembled in one country, shipped to another, and integrated into a facility under a separate EPC contract.
Test the supplier’s project-execution capability before award
Many delivery problems begin after the purchase order, when technical interfaces become real. Evaluate the project team that will execute the work, not just the business-development team that sold it. Review the proposed project manager, engineering leads, commissioning specialists, document-control process, change-management procedure, and escalation path.
Ask the supplier to walk through a sample project schedule with engineering deliverables, customer approval gates, procurement milestones, FAT dates, shipping sequence, site mobilization, SAT, and performance testing. The exercise should expose assumptions about grid connection, water treatment, foundations, cooling, nitrogen, vent routing, hydrogen offtake pressure, and control-system integration.
Spare-parts strategy is another practical test. A credible plan identifies commissioning spares, two-year operating spares, critical long-lead items, recommended stack-related inventory, storage conditions, and lead times. It should also explain who can diagnose faults, update software, authorize emergency work, and supply replacement components across borders.
Use contractual protections to convert evidence into accountability
Due diligence reduces uncertainty; contract structure determines who bears the remaining risk. Payments should be linked to verifiable milestones rather than broad statements of progress. Technical schedules should define performance guarantees, test methods, exclusions, liquidated damages where appropriate, warranty duration, availability commitments, defect remedies, and the process for resolving disputed test results.
For critical projects, consider independent inspection at key manufacturing stages and witness rights for FAT. Rights to review quality records, audit subcontractors, approve major design changes, and receive timely notice of supply-chain disruptions can be more valuable than a general promise of “priority service.”
When asking how to verify a supplier’s PEM electrolyzer delivery capability, the central discipline is to move from assertions to traceable proof. A credible supplier can show where its capacity comes from, which inputs constrain it, how quality is controlled, what comparable projects have actually achieved, and how risks are managed when conditions change. That evidence provides a sounder basis for a long-term hydrogen asset decision than capacity headlines alone.
Related News
- Electricity Price Volatility Is Rewriting Hydrogen Cost ModelsApr 27, 2026Impact of electricity price on hydrogen cost is transforming industrial decarbonization and large-scale electrolysis. Explore LCOH trends, PPA strategies, and resilient hydrogen infrastructure planning.
- Energy Transition Plans Often Fail at the Grid Connection StageApr 27, 2026Sustainable energy and energy transition projects often fail at grid connection. Learn how hydrogen infrastructure, PEM electrolysis, and industrial decarbonization can avoid delays and protect investment value.
- What Is Slowing Industrial Decarbonization Projects in 2026?Apr 27, 2026Industrial decarbonization faces delays in 2026 as hydrogen infrastructure, sustainable energy access, grid limits, safety standards, and project bankability challenge the energy transition.
- How G-HEI benchmarking can reveal PEM electrolyzer reliabilitySep 07, 2026G-HEI PEM electrolyzer benchmarking reliability reveals lifecycle risks, dynamic-duty performance, safety controls, and maintainability for smarter hydrogen investments.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.