
PEM Bipolar Plate Coating: What Determines Durability and Conductivity?




PEM Bipolar Plate Coating: What Determines Durability and Conductivity?
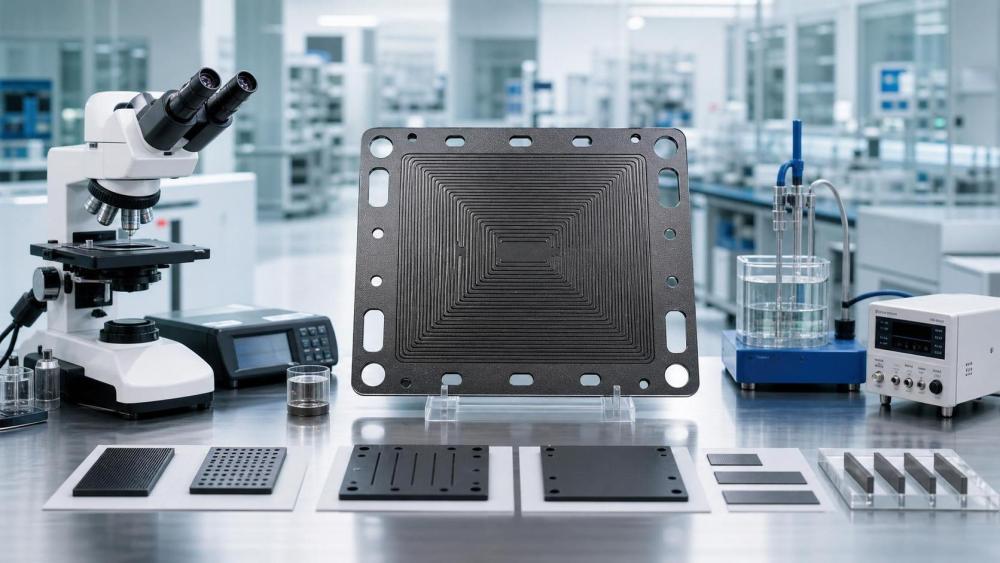
In PEM fuel cells and electrolyzers, PEM bipolar plate coating is never a secondary detail. It directly shapes corrosion resistance, contact resistance, and stack stability.
When current density rises and uptime targets tighten, coating performance becomes a system-level decision. Small surface failures can turn into measurable efficiency loss.
That is why PEM bipolar plate coating is closely reviewed in technical due diligence. Evaluators need proof of conductivity and proof of survival under real operating stress.
The core question is simple. What actually determines whether a coating remains conductive and durable over years, not only during lab qualification?
The answer sits at the intersection of substrate choice, coating chemistry, deposition quality, stack mechanics, and verification against recognized standards.
From a hydrogen infrastructure perspective, this matters even more. Sovereign-scale assets demand repeatable performance, not optimistic material claims.
Why PEM Bipolar Plate Coating Matters So Much
Bipolar plates guide gases, collect current, remove heat, and separate cells. Their coating must protect the plate while preserving low interfacial contact resistance.
In PEM environments, acidity, humidity, voltage cycling, and compression loads create a difficult operating window. Bare metals often fail quickly in that combination.
A suitable PEM bipolar plate coating reduces metal ion release, limits passive film growth, and keeps electron transfer efficient across the stack interface.
If conductivity drops, stack voltage rises. If corrosion starts, contamination can affect membranes, catalysts, and long-term reliability.
So the coating is not just a surface finish. It is a risk-control layer with direct implications for lifetime cost and bankability.
The Main Factors Behind Durability
Durability begins with chemistry, but it does not end there. A high-performing PEM bipolar plate coating depends on several linked factors.
1. Substrate Compatibility
Stainless steel is widely used for formed plates because it balances cost, strength, and manufacturability. Yet stainless steel needs a robust barrier against corrosion.
A coating may test well on polished coupons and still underperform on stamped flow fields. Surface roughness, alloy composition, and forming strain all matter.
2. Coating Material System
Common options include gold, titanium nitride, chromium nitride, amorphous carbon, graphite-like carbon, and multilayer systems. Each choice carries tradeoffs.
Nitrides can offer hardness and corrosion resistance. Carbon-based coatings often deliver strong conductivity, but pinhole control becomes critical.
Multilayer designs are increasingly relevant. They combine adhesion layers, diffusion barriers, and conductive top layers to improve lifetime stability.
3. Defect Density
Most failures start at defects. Pinholes, pores, microcracks, nodules, and edge damage create pathways for electrolyte access and localized attack.
Even a coating with excellent bulk properties can fail early if defect distribution is uncontrolled. This is a common blind spot in supplier qualification.
4. Adhesion Under Mechanical Stress
Stack assembly applies compression. Thermal cycling and pressure variation then add repeated stress.
If adhesion is weak, delamination follows. Once that starts, both durability and conductivity drop fast, especially at contact peaks and channel edges.
5. Operating Environment
Durability also depends on where the plate works. PEM fuel cells and PEM electrolyzers do not expose coatings to identical conditions.
Anodic potentials, startup conditions, humidity swings, fluoride species, and shutdown events can change corrosion behavior significantly.
What Controls Conductivity in Practice
Durability gets attention first, but conductivity often drives near-term system efficiency. The best PEM bipolar plate coating must stay electrically efficient over time.
Interfacial contact resistance, often called ICR, is the key metric. It reflects how easily current moves through the coated plate and adjacent gas diffusion layer.
Surface Chemistry and Passive Films
If the coating oxidizes or exposes the substrate, resistance rises. Passive films can be protective, but they are usually not helpful for low-contact electrical transfer.
Real Contact Area
Conductivity is not only a material property. It depends on how much of the rough surface truly touches the neighboring layer under compression.
This explains why a coating with impressive sheet conductivity may still show disappointing ICR inside a stack.
Thickness Optimization
Too thin, and defect risk increases. Too thick, and stress, cost, or electrical performance can worsen.
Strong PEM bipolar plate coating design usually finds a narrow process window where barrier function and low resistance both hold.
Compression Stability
A conductive coating must remain stable after repeated clamping and relaxation. Hardness helps, but brittleness can become a hidden failure trigger.
How Deposition Method Changes Performance
The same nominal coating chemistry can behave very differently depending on the deposition route. That is a decisive point in technical comparison.
PVD, PECVD, sputtering, arc processes, and hybrid treatments each produce different microstructures, residual stress levels, and defect patterns.
More importantly, scale-up can change the result. Pilot samples often look cleaner than high-throughput production parts.
In actual procurement, the relevant question is not only what process is used. It is whether that process is stable on formed geometries at production volume.
- Can the process coat deep channels uniformly?
- Are edges and corners protected?
- Does the line control contamination and thickness variation?
- Is there traceable lot data for corrosion and ICR results?
Which Tests Actually Prove a Coating
A credible PEM bipolar plate coating cannot be validated by one test. Decision-quality evidence needs combined electrochemical, mechanical, and surface data.
The best evaluations connect laboratory results with stack-relevant failure modes. That is where many datasheets fall short.
Where possible, test conditions should map to recognized industry expectations. References may include DOE targets, internal OEM protocols, and relevant ISO or ASTM methods.
For strategic hydrogen projects, traceability matters almost as much as performance. A result without process context has limited decision value.
Common Failure Modes to Watch Closely
Several patterns repeat across underperforming PEM bipolar plate coating programs. Spotting them early saves time and avoids expensive redesign cycles.
- Low initial ICR, followed by rapid drift after short corrosion exposure.
- Good coupon results, but poor behavior on stamped production plates.
- Edge attack near flow-field transitions and sealing zones.
- Adhesion loss after compression cycling or thermal shock.
- Supplier data based on idealized media, not relevant PEM duty conditions.
A more subtle issue is overreliance on average values. Coating durability is often determined by worst-case local defects, not batch averages.
A Practical Evaluation Framework
For procurement, design review, or asset benchmarking, it helps to assess PEM bipolar plate coating through a structured sequence.
- Confirm the substrate alloy, forming route, and surface preparation.
- Review coating architecture, including interlayers and target thickness.
- Check production capability on full geometry, not flat witness samples only.
- Compare corrosion and ICR data under relevant compressive loads.
- Request defect characterization and failure analysis evidence.
- Verify lot-to-lot consistency and scale manufacturing controls.
- Link material results to stack lifetime and maintenance assumptions.
This approach keeps attention on decision-grade facts. It also reduces the chance of choosing a coating that looks strong only in presentation slides.
Final Takeaway for Long-Life PEM Systems
A reliable PEM bipolar plate coating is defined by balance. It must resist corrosion, maintain low contact resistance, adhere under stress, and scale into production.
No single metric can prove that balance. The strongest decisions come from linking coating chemistry, process control, defect analysis, and stack-relevant testing.
As hydrogen infrastructure moves toward larger, sovereign-grade deployment, surface engineering becomes a strategic reliability issue. That shifts PEM bipolar plate coating from component detail to investment-critical parameter.
The practical path is clear: evaluate the coating as a full operating system, not a standalone material label. That is usually where durable performance is either proven or exposed.
Related News
- Electricity Price Volatility Is Rewriting Hydrogen Cost ModelsApr 27, 2026Impact of electricity price on hydrogen cost is transforming industrial decarbonization and large-scale electrolysis. Explore LCOH trends, PPA strategies, and resilient hydrogen infrastructure planning.
- Energy Transition Plans Often Fail at the Grid Connection StageApr 27, 2026Sustainable energy and energy transition projects often fail at grid connection. Learn how hydrogen infrastructure, PEM electrolysis, and industrial decarbonization can avoid delays and protect investment value.
- What Is Slowing Industrial Decarbonization Projects in 2026?Apr 27, 2026Industrial decarbonization faces delays in 2026 as hydrogen infrastructure, sustainable energy access, grid limits, safety standards, and project bankability challenge the energy transition.
- How G-HEI benchmarking can reveal PEM electrolyzer reliabilitySep 07, 2026G-HEI PEM electrolyzer benchmarking reliability reveals lifecycle risks, dynamic-duty performance, safety controls, and maintainability for smarter hydrogen investments.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.