
PEM Water Electrolysis High Purity: What Determines Output Quality?




PEM water electrolysis high purity is often discussed as a hydrogen specification, yet output quality is really the result of an entire operating system. In large-scale infrastructure, purity depends on stack design, water treatment, gas crossover control, pressure strategy, and the way purification is integrated after the electrolyzer. That is why this topic now matters far beyond laboratory performance claims.
As hydrogen projects move into sovereign-scale energy planning, purity affects safety, compression reliability, fuel cell compatibility, storage integrity, and regulatory acceptance. Within the broader benchmarking work of G-HEI, PEM water electrolysis high purity sits at the junction of electrolysis performance, materials discipline, and downstream asset security.
Why output quality has become a strategic issue
Hydrogen markets are no longer shaped only by production cost. They are increasingly shaped by whether produced hydrogen can move through compression, liquefaction, pipeline blending, refueling, or turbine use without creating contamination risk.
That shift changes the way PEM water electrolysis high purity should be evaluated. A plant may show acceptable nameplate output, but still create downstream losses if oxygen, moisture, particulates, or ionic contaminants remain unstable.
This is especially relevant in projects benchmarked against strict frameworks such as ISO 19880, ASME B31.12, and SAE J2601, where hydrogen quality connects directly to system safety and operating confidence.
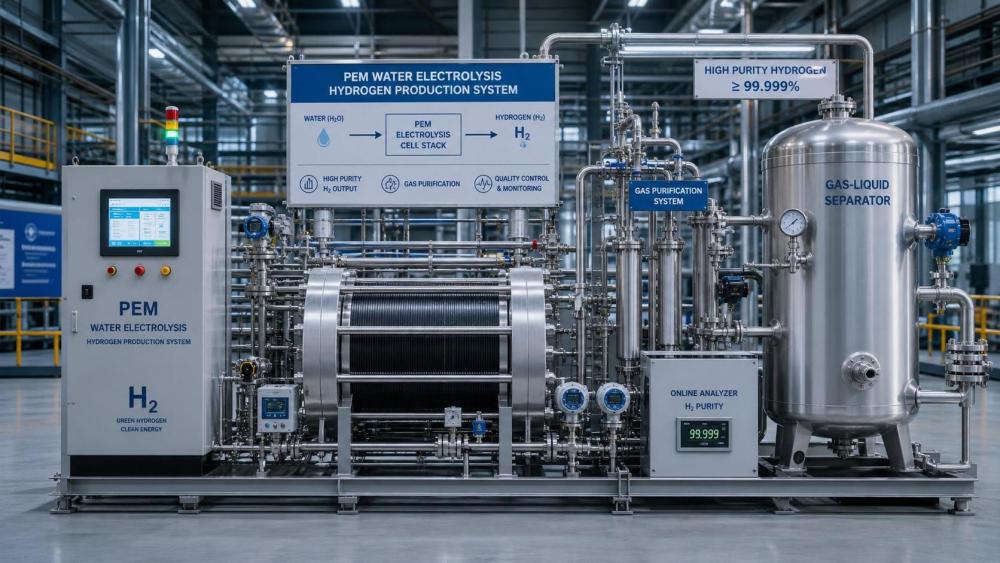
The issue is not simply whether hydrogen is pure at startup. The more important question is whether purity remains stable across load swings, seasonal water variability, pressure changes, and stack aging.
What PEM water electrolysis high purity really means
In practical terms, high purity refers to hydrogen with tightly controlled impurity levels at the outlet condition required by its end use. The exact threshold depends on whether the hydrogen goes to storage, mobility, industrial feedstock, or power conversion.
PEM systems are often favored because they can produce high-purity hydrogen directly, with fast dynamic response and compact plant layout. However, inherent purity potential is not the same as guaranteed delivered purity.
A useful evaluation starts by separating three questions: stack outlet purity, conditioned gas purity, and delivered hydrogen purity at the transfer boundary. Many project documents blur these stages and create false confidence.
Purity is shaped by more than one boundary
At the stack outlet, concern centers on oxygen crossover, moisture, and traces related to membrane and catalyst conditions. After separation, the concern shifts toward dryers, deoxo units, filters, valves, and storage interaction.
By the custody transfer point, material cleanliness, seal integrity, and sampling discipline may matter as much as the electrolyzer itself. This is where many PEM water electrolysis high purity claims need closer scrutiny.
The main variables that determine output quality
Several technical variables repeatedly determine whether PEM water electrolysis high purity remains consistent in real facilities rather than only in vendor literature.
1. Water quality and polishing stability
PEM electrolyzers require highly purified feedwater. Variations in conductivity, silica, organics, chlorides, or metallic ions can degrade membrane behavior and accelerate contamination pathways.
More important than inlet specification alone is the consistency of the polishing loop. A plant with nominally pure water but unstable resin performance can experience gradual purity drift.
2. Stack materials and membrane condition
Titanium hardware, catalyst layers, membrane quality, and sealing materials all influence contamination behavior. Material choices affect corrosion resistance, ion release, and long-term gas separation efficiency.
As stacks age, microdefects, compression changes, and chemical stress can increase crossover. High initial purity therefore says little unless it is paired with durability evidence.
3. Operating pressure and load profile
Pressure helps reduce downstream compression work, but it also changes gas transport behavior across the membrane and separation equipment. Transient operation can intensify these effects.
Facilities following variable renewable power profiles often cycle more aggressively. Under those conditions, PEM water electrolysis high purity should be verified during ramping, turndown, and restart, not only at steady state.
4. Gas-liquid separation and oxygen management
Hydrogen purity depends heavily on the quality of phase separation after electrolysis. Poor separator design or unstable controls can allow entrained moisture and oxygen carryover to persist.
This has direct safety implications. Oxygen contamination is not only a quality issue; it also affects compression equipment, storage compatibility, and hazardous area design assumptions.
5. Downstream purification architecture
Many projects rely on dryers, catalytic deoxygenation, particulate filtration, and polishing stages to meet final purity targets. The design logic of this train matters more than the presence of equipment alone.
A well-designed system accounts for upset conditions, maintenance intervals, bypass risks, and analyzer placement. Without that discipline, PEM water electrolysis high purity becomes a conditional outcome rather than a reliable one.
How quality requirements change by application
Not every hydrogen pathway requires the same purity envelope. The right benchmark depends on the downstream asset and the consequences of contamination.
This variation explains why one purity statement cannot serve every commercial decision. In integrated infrastructure, hydrogen quality must be judged against the full value chain, not only electrolyzer output.
What to examine during technical benchmarking
In practice, a strong review of PEM water electrolysis high purity should test claims under operating realism. It should also connect purity data to standards, maintenance, and asset interfaces.
- Check whether purity values are reported at stack outlet, after purification, or at delivery boundary.
- Review impurity profiles, not just total purity percentages.
- Look for data across load changes, startups, shutdowns, and degraded water conditions.
- Confirm analyzer type, calibration frequency, sampling location, and response time.
- Assess how stack aging affects crossover and whether replacement criteria are defined.
- Verify compatibility between produced hydrogen quality and downstream compression, storage, or refueling assets.
Benchmarking organizations such as G-HEI add value here by comparing equipment claims against international frameworks and real asset behavior. That broader context is essential when purity becomes a system-risk variable.
Common mistakes in interpreting purity performance
One common mistake is assuming PEM technology automatically guarantees final-use purity without substantial downstream conditioning. Another is treating occasional lab samples as evidence of plant-wide reliability.
There is also a tendency to focus on headline efficiency while underweighting contamination control. In many infrastructure cases, low impurity variability is more valuable than marginal efficiency gains.
A final issue is disconnected procurement. Stack suppliers, purification vendors, compressor packages, and storage designers may optimize their own scope while leaving purity accountability fragmented.
Where the next decisions should focus
PEM water electrolysis high purity should be treated as a chain of verified conditions, not a single advertised attribute. The most useful next step is to map purity requirements backward from the final application.
That means defining the delivery boundary, identifying unacceptable contaminants, testing dynamic operating cases, and checking how standards apply across production, transport, and use.
Where project stakes are high, it is worth building a benchmark set that links stack materials, water treatment discipline, gas separation efficiency, and downstream purification into one decision framework. That is usually where output quality becomes clear, comparable, and actionable.
Related News
- Electricity Price Volatility Is Rewriting Hydrogen Cost ModelsApr 27, 2026Impact of electricity price on hydrogen cost is transforming industrial decarbonization and large-scale electrolysis. Explore LCOH trends, PPA strategies, and resilient hydrogen infrastructure planning.
- Energy Transition Plans Often Fail at the Grid Connection StageApr 27, 2026Sustainable energy and energy transition projects often fail at grid connection. Learn how hydrogen infrastructure, PEM electrolysis, and industrial decarbonization can avoid delays and protect investment value.
- What Is Slowing Industrial Decarbonization Projects in 2026?Apr 27, 2026Industrial decarbonization faces delays in 2026 as hydrogen infrastructure, sustainable energy access, grid limits, safety standards, and project bankability challenge the energy transition.
- How G-HEI benchmarking can reveal PEM electrolyzer reliabilitySep 07, 2026G-HEI PEM electrolyzer benchmarking reliability reveals lifecycle risks, dynamic-duty performance, safety controls, and maintainability for smarter hydrogen investments.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.