When does bipolar plate coating technology improve PEM electrolyzer durability?




Bipolar plate coating technology improves PEM electrolyzer durability when the uncoated plate would otherwise become the dominant source of corrosion products, interfacial resistance drift, or localized shutdown risk. In practical terms, that threshold is usually reached under acidic, deionized-water service at elevated current density, frequent load changes, warm stack temperatures, and long operating windows where even small material losses can contaminate the membrane-electrode assembly. A coating matters most when it preserves both chemical stability and low contact resistance under compression, because durability in this part of the stack is rarely a single-variable problem.
The baseline material decides whether coating is an enhancement or a necessity. Titanium already offers strong corrosion resistance in PEM environments, but its native oxide film increases interfacial contact resistance. Stainless steel can offer attractive forming and cost characteristics, yet in anodic conditions it may require a far more demanding surface strategy to avoid metal ion release and rapid passivation-related losses. A coating therefore improves durability only if it addresses the actual weakness of the substrate. On titanium, that often means managing conductivity without undermining corrosion behavior. On steel, the task is usually broader: limiting dissolution, protecting defect sites, and preventing the stack from accumulating contamination that later appears as voltage rise or uneven cell aging.
Many durability problems attributed to membranes or catalysts begin at the plate surface. If a coating develops pinholes, edge thinning, or poor adhesion around flow-field corners, the exposed substrate can create local galvanic or oxidative attack. That attack may remain invisible during short qualification tests, especially if average cell voltage still looks acceptable. The improvement becomes meaningful when the coating remains intact through compression, thermal cycling, hydration changes, and start-stop transients. A decorative or nominally conductive film that cannot survive these mechanical and electrochemical stresses does little for stack life, even if its initial laboratory resistance values are excellent.
Where coating changes the failure trajectory
The strongest case for bipolar plate coating technology appears in the anode-side environment of PEM electrolysis, where oxygen evolution, low pH conditions near the catalyst layer, and oxidizing potentials combine to challenge exposed metallic surfaces. In that setting, a suitable coating can slow three linked degradation routes at once: growth of electrically resistive oxides, release of dissolved species into the water path, and roughening of the contact interface under clamping pressure. When those routes are suppressed, stack aging often becomes more predictable because one source of coupled electrochemical and mechanical instability has been removed.
Improvement is also pronounced in stacks designed for dynamic operation. Systems tied to variable power input may experience repeated ramping, standby intervals, and restarts. Each transient can disturb water distribution, change local potential exposure, and shift thermal gradients across the plate. Coatings that perform well only at constant-state polarization may crack or chemically transform during these transitions. A robust coating adds value when it tolerates these non-steady conditions without a rapid increase in contact resistance or visible flaking at channel lands and gasket-adjacent regions.
Another condition is high compaction demand. Bipolar plates must maintain electrical contact while sealing against leakage, which means the coating sits in a mechanically loaded interface rather than a purely chemical environment. If the chosen film is brittle, too thick, or poorly bonded, compressive loading can generate microfractures that later become corrosion entry points. Durability improves when the coating architecture accounts for both hardness and compliance, especially on stamped or formed plates where strain may already be locked into the substrate before coating deposition begins.
What the coating must actually do
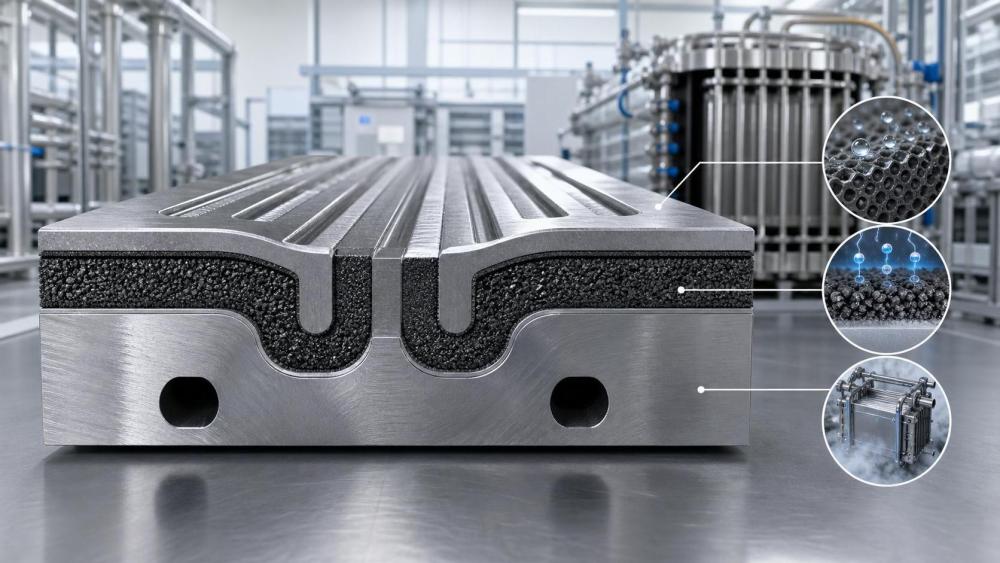
A useful coating for PEM bipolar plates is expected to satisfy several demands at once, but they are not all equally difficult. Low interfacial contact resistance is often straightforward at the start of life; maintaining it after polarization, compression, and wet exposure is harder. Corrosion resistance can also look strong in simple immersion tests while failing in real stack duty because the electrochemical potential and contact pressure are different. The durability benefit appears only when the film maintains function in the assembled state, not just as a coupon in an isolated test cell.
Conductive nitrides, carbides, noble-metal-containing layers, and multi-layer barrier systems are often discussed because each addresses a different balance of conductivity, hardness, porosity, and chemical stability. A very conductive layer can still underperform if it is columnar and porous. A very inert barrier can still be problematic if it raises contact resistance enough to increase heat generation at the interface. Multi-layer designs can be effective where a base adhesion layer, a corrosion barrier, and a conductive top layer are carefully matched, but they can also fail at internal interfaces if thermal expansion mismatch or residual stress is ignored.
Thickness control deserves more attention than it usually gets in procurement discussions. Excess thickness may increase crack sensitivity, create edge coverage problems, or raise deposition time and rejection rates. Insufficient thickness may leave asperity peaks underprotected, especially after forming and compression flatten the contact lands. The most durable outcome is often tied to the process window rather than the nominal coating chemistry alone. A narrow process that works only on ideal coupons can become unreliable once full-size plates with sharp radii, manifold openings, and variable surface roughness enter production.
Why some coatings test well and still disappoint in service
A common misjudgment is to treat corrosion current data from a polished flat sample as a direct predictor of stack durability. Real bipolar plates include channels, lands, edges, pierced holes, weld-adjacent zones in some assemblies, and deformation from stamping or hydroforming. These features influence coating continuity and local stress. If qualification ignores them, the resulting plate can pass basic electrochemical screening while still failing first at cut edges or around geometric transitions where deposition shadowing occurred.
Another weak point is edge management. Even a high-quality coating may leave the perimeter, header region, or threaded attachment features more vulnerable than the main flow field. In PEM service, those locations can become initiation points for crevice-type corrosion or contamination release, especially if the sealing system traps water and dissolved oxygen in stagnant pockets during shutdown. Durability improves when the coating strategy is integrated with plate finishing, edge treatment, cleaning, and gasket design, not chosen as an isolated material decision.
Handling damage is often underestimated. Coated plates may leave the deposition line in good condition and then lose performance because of contact scratches, rack marks, particle embedding, or stacking abrasion during transport and assembly. Since many coatings are thin, a small scar can expose substrate and create a local failure site out of proportion to its size. The value of bipolar plate coating technology therefore depends partly on how the supply chain protects surfaces after deposition. Tray materials, separator films, glove cleanliness, and allowable touch points are part of durability control whether or not they appear in the material specification.
Operating conditions that justify tighter coating requirements
More stringent coating performance is usually warranted when the stack is expected to run at elevated differential pressure, high outlet gas purity requirements, or long maintenance intervals. Under these conditions, a small rise in metal contamination risk or interfacial resistance can propagate into wider system concerns such as water-loop cleanliness, separator loading, or diagnostic ambiguity during fault analysis. A coating can materially improve durability when it reduces those secondary effects and keeps plate-related degradation from masking other stack behavior.
Water quality also changes the value proposition. PEM systems are typically supplied with highly purified water, but excursions in ionic cleanliness during startup, maintenance, or component replacement can alter corrosion behavior at exposed defects. A more robust coating architecture offers resilience against these off-design moments. That does not make poor water management acceptable; it means the plate surface is less likely to become the first casualty when water chemistry temporarily drifts.
Thermal distribution matters as well. Plates near the edges of a stack or in zones with less uniform cooling may experience different stress histories than central cells. If the selected coating has marginal adhesion, repeated warm-cool cycling can cause subtle delamination that remains electrically tolerable for some time before accelerating. In such cases the coating improves durability only if it has been validated under representative thermal gradients and compression maps rather than average stack temperature alone.
Manufacturing and inspection details that separate durable coatings from nominal ones
Surface preparation usually determines whether a coating becomes a long-term asset or an expensive variable. Oils from forming, embedded abrasives, native oxides of inconsistent thickness, and residual alkaline cleaners all interfere with adhesion. A disciplined route might include degreasing, oxide conditioning, controlled roughness preparation, rinsing with low-residue chemistry, and strict drying before deposition. If those steps vary between batches, durability scatter can widen enough that the coating’s average performance stops being useful.
Deposition method selection should follow geometry and failure mode, not fashion. Physical vapor deposition may offer dense, conductive films with good thickness control, but line-of-sight limitations can challenge recessed features. Electrochemical or electroless routes may improve coverage in some geometries while introducing their own bath-control issues. Thermal spray is generally too coarse for many PEM plate interfaces unless followed by substantial finishing and sealing steps. The durable choice is the one that reliably covers the full functional area, including channel roots and transition radii, with manageable residual stress.
Inspection should look beyond visual appearance. Useful release criteria often include contact resistance under representative compression, corrosion testing at relevant potentials, adhesion or scratch resistance, porosity assessment, thickness mapping across complex features, and contamination analysis from the finished surface. Cross-sectional microscopy can reveal voids or interface defects that average electrical tests miss. If a supplier can report only nominal chemistry and mean thickness, that is usually too little information for a component expected to survive aggressive electrochemical duty.
When coating may add complexity without enough durability gain
There are cases where coating offers limited benefit. If the stack architecture already uses a substrate whose passive behavior and contact interface are acceptable for the intended duty, adding a coating may simply introduce another failure mechanism. The same caution applies when operating conditions are relatively mild, current density is modest, maintenance intervals are short, or replacement economics tolerate plate turnover. In those circumstances, the durability gain from coating may be small compared with the added burden of process control, inspection, repair handling, and supplier qualification.
Coating can also be the wrong answer when the observed problem is actually rooted in stack compression nonuniformity, water maldistribution, or contamination introduced elsewhere in the balance of plant. A low-quality interface can resemble coating failure because both appear as voltage instability and localized degradation. Before changing the plate surface, it is worth isolating whether the interface is being damaged by mechanical overloading, particulate ingress, seal creep, or assembly distortion. Otherwise, a new coating may be blamed for a system-level defect it did not create.
The point at which bipolar plate coating technology improves PEM electrolyzer durability is therefore not defined by coating presence alone. It is defined by whether the coating remains conductive, adherent, chemically stable, and manufacturable across the full life of the compressed stack, including shutdowns, ramps, cleaning events, and handling between factory and field. When those conditions are met, the coating can shift plate behavior from a latent degradation source to a controlled interface. When they are not, the coating becomes another variable that complicates qualification without extending service life in a meaningful way.
Related News
- Electricity Price Volatility Is Rewriting Hydrogen Cost ModelsApr 27, 2026Impact of electricity price on hydrogen cost is transforming industrial decarbonization and large-scale electrolysis. Explore LCOH trends, PPA strategies, and resilient hydrogen infrastructure planning.
- Energy Transition Plans Often Fail at the Grid Connection StageApr 27, 2026Sustainable energy and energy transition projects often fail at grid connection. Learn how hydrogen infrastructure, PEM electrolysis, and industrial decarbonization can avoid delays and protect investment value.
- What Is Slowing Industrial Decarbonization Projects in 2026?Apr 27, 2026Industrial decarbonization faces delays in 2026 as hydrogen infrastructure, sustainable energy access, grid limits, safety standards, and project bankability challenge the energy transition.
- How G-HEI benchmarking can reveal PEM electrolyzer reliabilitySep 07, 2026G-HEI PEM electrolyzer benchmarking reliability reveals lifecycle risks, dynamic-duty performance, safety controls, and maintainability for smarter hydrogen investments.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Aris Aero
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.