
Precision Manufacturing: 7 Quality Risks That Delay Hydrogen Equipment Delivery




Precision Manufacturing: 7 Quality Risks That Delay Hydrogen Equipment Delivery
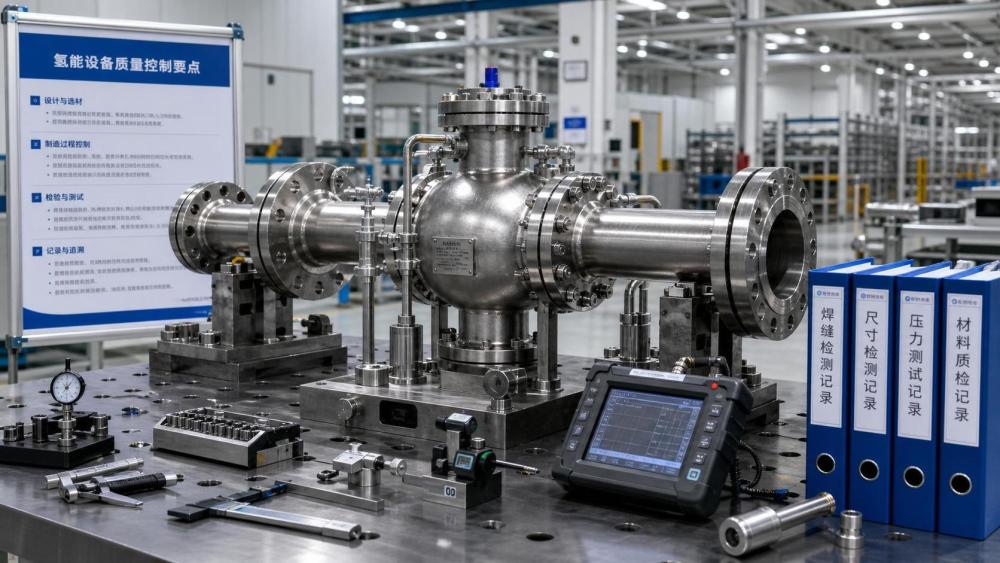
In hydrogen equipment projects, precision manufacturing is rarely just about machining accuracy.
It directly affects delivery timing, certification progress, and operating safety.
That pressure is even higher in electrolysis skids, cryogenic vessels, and 70MPa refueling systems.
A small manufacturing deviation can trigger retesting, NCR escalation, or shipment holds.
From a project-control view, precision manufacturing is a schedule protection tool.
From a safety view, it is a barrier against leaks, embrittlement, fatigue, and compliance gaps.
The seven risks below show where hydrogen equipment programs most often lose time.
More importantly, they show how precision manufacturing can keep delivery plans intact.
1. Material Traceability Breaks Before Fabrication Starts
Many delays begin long before welding, machining, or pressure testing.
They start when raw materials lose clear traceability across receiving, storage, and cutting operations.
In hydrogen service, this is not a paperwork issue.
It affects alloy verification, heat treatment history, and suitability for pressure or cryogenic duty.
If a PMI mismatch appears late, the part may need full quarantine.
That usually means rework, replacement procurement, and witness delays.
- Use heat-level traceability from goods receipt to final assembly.
- Separate hydrogen-critical materials from general inventory.
- Tie MTCs, PMI records, and cut-piece IDs to one digital lot history.
2. Machining Tolerances Drift Beyond Functional Limits
Hydrogen equipment often depends on tight interfaces.
Seal grooves, flange faces, valve seats, and stack components leave little room for dimensional variation.
When tolerance drift goes unnoticed, assembly may still appear possible.
The real problem shows up later as leakage, vibration, or unstable pressure behavior.
Precision manufacturing must therefore focus on functional geometry, not only nominal dimensions.
Critical-to-quality characteristics need a stricter control plan than standard shop parts.
In practice, late dimensional findings can stop FAT readiness immediately.
- Define CTQ dimensions at drawing release, not after first article inspection.
- Use calibrated fixtures and MSA-reviewed measurement methods.
- Trigger containment when process capability weakens on hydrogen-critical features.
3. Welding Variables Are Controlled on Paper, Not on the Floor
This is one of the most persistent quality risks in pressure equipment manufacturing.
Approved WPS and PQR packages may exist, yet real welding conditions still drift.
Travel speed, interpass temperature, filler handling, and purge quality often decide the outcome.
For hydrogen systems, poor weld execution raises the risk of cracking and permeability problems.
That becomes especially serious in stainless tubing, nozzles, manifolds, and thick-wall pressure parts.
Once repair rates rise, delivery dates usually move with them.
Precision manufacturing depends on disciplined weld variable control at every shift, not just audit time.
- Verify welder continuity and process qualification before hydrogen-critical jobs.
- Monitor purge quality and consumable storage as production controls.
- Review repair trends weekly to catch process instability early.
4. Surface Cleanliness Is Treated as Cosmetic, Not Functional
In hydrogen equipment, cleanliness has performance and safety consequences.
Residual oil, embedded iron, moisture, and abrasive particles can compromise service integrity.
This matters in compressors, valve blocks, electrolysis balance-of-plant assemblies, and cryogenic lines.
A component can meet dimensions and still fail project expectations because contamination was ignored.
More noticeably now, clients ask for documented cleaning acceptance, not verbal confirmation.
That shift is changing how precision manufacturing programs prepare for inspection release.
If cleanliness is checked too late, packaging and preservation may need to be repeated.
What to tighten immediately
- Define cleanliness criteria by service condition and media sensitivity.
- Separate carbon steel and stainless processing areas where possible.
- Add documented final cleaning and borescope checks before closure.
5. NDT Planning Happens After Production, Not During It
Non-destructive testing should support flow, not interrupt it.
Yet many projects still schedule RT, UT, PT, or helium leak testing too late.
The result is predictable.
Assemblies wait for access, coatings block inspection, or witness dates slip.
For hydrogen packages, NDT timing also affects code compliance evidence.
If inspection hold points are missed, certification review can stall despite completed fabrication.
Precision manufacturing needs inspection sequencing built into the traveler from day one.
6. Supplier Quality Is Monitored by Documents Alone
Hydrogen projects depend on specialist suppliers for forgings, valves, seals, tubing, and instrumentation.
The risk appears when incoming quality looks compliant only because the paperwork looks complete.
Certificates alone do not confirm process consistency.
They also do not reveal packaging damage, preservation failure, or unauthorized substitutions.
In real projects, supplier escapes often surface during assembly or leak testing.
By then, replacement lead times can wreck a delivery plan.
Precision manufacturing requires supplier control that reaches beyond document collection.
- Rank suppliers by hydrogen service criticality, not only spend level.
- Increase source inspection for pressure-boundary and sealing components.
- Track supplier escapes by failure mode and project impact.
7. Final Documentation Lags Behind Physical Completion
This is a quiet but expensive cause of delayed shipment.
The unit is built, tested, preserved, and ready to move.
But the document package is still missing weld maps, calibration records, or signed release points.
For regulated hydrogen assets, that gap can be enough to block handover.
This matters across ISO 19880, ASME B31.12, SAE J2601, and related client specifications.
More projects now fail schedule targets because records were treated as an afterthought.
Strong precision manufacturing includes dossier readiness as part of production control.
A practical closeout routine
- Collect quality records at each operation, not at project close.
- Review turnover packs weekly against the ITP and contract matrix.
- Hold shipment release until physical status and dossier status match.
How to Reduce Delay Risk Across the Full Manufacturing Chain
The common thread across these seven risks is control timing.
Problems become expensive when precision manufacturing controls start after variation already spreads.
That is why leading hydrogen programs combine process discipline with early risk visibility.
Within G-HEI benchmarking, the strongest performers do three things consistently.
- They define hydrogen-critical quality points before procurement and release.
- They connect inspection evidence to schedule decisions in real time.
- They treat precision manufacturing as a reliability and compliance system.
That approach fits the current hydrogen economy transition.
As assets scale from pilot units to sovereign infrastructure, tolerance for avoidable delay keeps shrinking.
A disciplined precision manufacturing strategy helps prevent both technical drift and project drag.
If delivery certainty matters, start by auditing these seven risk points against current workflows.
That review usually reveals the fastest path to stronger quality, safer assets, and fewer shipment surprises.
Related News
- When 99.999% Hydrogen Purity Still Is Not Good EnoughApr 27, 2026Industrial decarbonization starts with more than hydrogen gas purity (99.999%). Explore hydrogen infrastructure, material integrity, safety standards, and utility-scale performance risks.
- PSA Recovery Rate Drops for Reasons Operators MissApr 27, 2026Pressure swing adsorption (PSA) recovery rate drops often stem from hidden control, valve, and adsorbent issues—not feed gas alone. Learn how to protect hydrogen purity, storage efficiency, and industrial decarbonization performance.
- Which hydrogen procurement standards verify fuel quality at refueling stations?Aug 29, 2026Hydrogen procurement standards explained: learn how ISO 14687, SAE J2719, ISO 19880, and SAE J2601 verify fuel quality, station controls, and safe 70 MPa refueling.
- EU Mandates ISO 19880-5 Sensors for 70MPa Hydrogen StationsAug 14, 2026ISO 19880-5 sensors are now mandatory for EU 70MPa hydrogen stations. See what the new rule means for suppliers, integrators, and compliance-ready projects.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Victor Gear
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.