
Titanium Bipolar Plate Coating Thickness Specifications for Corrosion Resistance




It often starts with a specification sheet that looks complete at first glance. A team is reviewing components for a PEM stack, the substrate is titanium, the coating is described in broad terms, and the corrosion target seems covered. Then the practical questions show up: Is the coating thick enough to survive the acidic, high-potential environment? Is it too thick for stable contact resistance? Can incoming inspection actually verify what the supplier claims? That is where titanium bipolar plate coating thickness specifications stop being a paperwork detail and become a reliability decision.
This issue is frustrating because the failure mode is rarely obvious on day one. A plate can appear acceptable during procurement review, yet later create higher interfacial losses, local coating defects, or corrosion concerns that are hard to separate from other stack problems. In hydrogen systems, especially where uptime, safety review, and long service intervals matter, a vague thickness range leaves too much room for interpretation. Many technical evaluators run into the same problem: the drawing says one thing, the process capability suggests another, and the validation method does not fully match the application.
Where the confusion usually begins
A common misunderstanding is to treat coating thickness as a single-pass/fail number. In practice, it is tied to at least three interacting requirements: corrosion resistance, electrical contact behavior, and manufacturing consistency across a complex flow field surface. A titanium bipolar plate in PEM service is not simply “better” because the coating is thicker. If the coating system is based on a precious metal, nitride, carbide, or a multilayer conductive barrier, the useful thickness window depends on coating density, adhesion, pore structure, deposition method, and where the plate will actually see the highest electrochemical stress.
Another source of trouble is that thickness values are sometimes borrowed from a different stack design, a different duty cycle, or even a different test philosophy. A lab coupon with a flat polished surface does not behave exactly like a formed bipolar plate with channels, edges, lands, and handling marks. The specification therefore has to describe more than nominal thickness. It should also define where the measurement applies, what local minimum is acceptable, and which verification method is valid.
Why thickness cannot be separated from the coating system
When engineers ask for titanium bipolar plate coating thickness specifications, they are usually trying to answer a broader question: what thickness range is sufficient to create a durable conductive barrier without introducing unnecessary process risk? The answer depends on the coating family.
For noble-metal-based coatings, very thin layers may provide excellent conductivity, but continuity and defect sensitivity become critical. Pinholes, edge thinning, or incomplete coverage can expose titanium to the PEM environment, especially under repeated startup, shutdown, and load variation. In that case, the “right” thickness is not just the average deposited amount. It is the thickness at the weakest locations after forming, cleaning, coating, and handling.
For ceramic-like conductive coatings such as nitrides or carbides, a larger thickness may improve barrier performance, yet internal stress, brittleness, and adhesion become part of the decision. If the layer is too stressed, cracking at formed features or under clamping load can undermine the corrosion target. A thicker layer that fractures is not safer than a thinner layer that remains intact.
That is why reviewing a thickness figure without the associated deposition route is risky. PVD, CVD, electroplating, thermal processes, and hybrid approaches leave different microstructures. Two suppliers may quote the same nominal thickness and still deliver very different plate behavior.
The practical way to write a usable specification
If you are building or reviewing a drawing, the most useful approach is to specify a thickness window rather than a single ideal number, then tie that window to function. A usable document normally addresses five points.
1. State the substrate condition before coating
Titanium surface preparation affects adhesion and the measured coating profile. If cleaning, etching, roughening, or passivation steps are not controlled, thickness results can look inconsistent even when the deposition itself is stable. The specification should reference the required pre-coating surface state, not only the final layer.
2. Separate nominal thickness from local minimum thickness
This is one of the most important corrections to weak documents. Nominal thickness may describe the target process setting, while local minimum thickness protects the part in service. Without a local minimum requirement, thin zones on edges, channel roots, or corners can be missed.
3. Define the measurement method
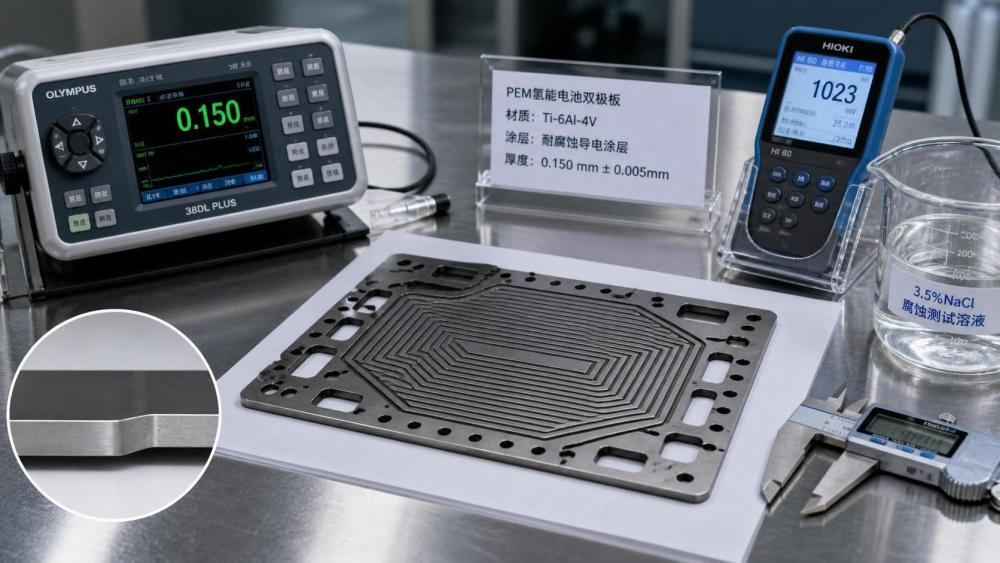
Cross-section microscopy, XRF, eddy-current methods, profilometry, and weight-gain approaches do not always produce directly interchangeable values. On shaped titanium bipolar plates, method limitations matter. If the supplier reports thickness by one method and incoming quality verifies by another, disputes are almost guaranteed.
4. Identify measurement locations
A flat witness coupon can be useful for process monitoring, but it should not fully replace part-based verification. Thickness should be checked at representative lands, channels, transition radii, and edge regions whenever the geometry makes those areas vulnerable.
5. Link thickness to post-coating performance checks
A thickness requirement alone is incomplete. It should sit alongside contact resistance criteria, adhesion expectations, and corrosion test conditions relevant to PEM operation. A plate can meet thickness and still fail function.
What usually goes wrong during verification
One recurring problem is overreliance on average values. An average thickness report can hide local discontinuities. For corrosion resistance, local defects usually matter more than the arithmetic mean. Another problem is specifying a coating thickness that is theoretically desirable but difficult to reproduce consistently over production geometry. That tends to create drift between pilot parts and scale-up lots.
There is also a tendency to compare supplier data without normalizing the basis of comparison. One supplier may report thickness on witness samples, another on production plates, and another as a process target rather than measured output. If these are treated as equivalent, the review can become misleading very quickly.
Handling damage is easy to underestimate as well. Even when the deposited layer meets the drawing, stacking, fixturing, masking, cleaning, or post-coating assembly contact can alter the effective protective thickness in local areas. For that reason, a good specification often includes acceptance logic for cosmetic marks versus functional damage, rather than leaving the decision to visual judgment alone.
A more reliable decision path for technical review
When a coating proposal lands on your desk, it helps to resist the urge to ask only, “What is the thickness?” A better sequence is narrower and more useful.
Start with the service environment. PEM bipolar plates see a combination of acidity, electrical potential, compression, humidity cycling, and mechanical contact. The coating must remain conductive while preventing unacceptable substrate interaction. This frames whether the coating system should prioritize ultralow contact resistance, stronger barrier behavior, or a balance of both.
Next, look at the plate geometry and manufacturing route. A simple flat sample can support screening work, but production plates with flow fields are where thickness control becomes real. Formed features influence line-of-sight deposition, shadowing, and edge behavior. If the process cannot deliver adequate coverage in these regions, the nominal number on the quote does not help much.
Then review the supplier’s thickness evidence. Ask whether results come from witness coupons, destructively sectioned parts, or non-destructive scans on production surfaces. Ask how many locations were measured and whether the report distinguishes average from minimum. This is often where unclear specifications become visible.
After that, connect the thickness range to corrosion and interfacial contact resistance testing. The point is not to demand excessive testing for its own sake. It is to make sure the thickness figure represents a coating that has already been checked under conditions resembling the intended use. If the coating only performs on a flat test coupon, the specification is not mature enough.
When “thicker is safer” leads to the wrong conclusion
Many buyers and reviewers instinctively lean toward thicker coatings because corrosion feels like a barrier problem. The instinct is understandable, but it can be incomplete. Some coating systems gain little practical advantage once continuity and defect control are achieved, while extra thickness may raise cost, internal stress, process time, or variation between locations on the plate.
For conductive surface systems used on titanium bipolar plates, the better question is whether the selected thickness remains stable within the combined electrical and chemical demands of the stack. If a thinner, well-adhered, low-defect layer consistently meets corrosion and contact targets, increasing thickness may not improve the outcome. On the other hand, if the process window is narrow and local thinning is common, a somewhat higher nominal target may be justified simply to maintain the local minimum.
That is why the specification should reflect process capability, not just idealized material preference. A range grounded in repeatable deposition behavior is usually more valuable than a very tight number that only works under perfect conditions.
How to reduce disagreement between procurement, quality, and engineering
Thickness disputes often happen because each group is solving a different problem. Procurement wants a comparable quote. Quality wants measurable acceptance criteria. Engineering wants confidence in stack performance. The document has to satisfy all three without turning into a research paper.
A practical way to do that is to keep the drawing concise and move the test logic into a controlled material or process specification. The drawing can identify the approved coating system, the nominal thickness range, the minimum local thickness, and any protected surfaces. The supporting specification can define preparation, deposition method, witness sample rules, verification locations, and the correlation between thickness and functional tests.
This split also helps when a technical hub or internal benchmarking team is comparing candidate plate technologies. Instead of arguing over isolated thickness numbers, reviewers can compare thickness in context: substrate state, coating class, verification method, and expected PEM duty.
Questions worth asking before approving a coating thickness range
If you are close to a decision, a few grounded questions tend to reveal whether the specification is robust enough:
- Does the range reflect the actual deposition process on formed titanium plates, not just coupons?
- Is there a defined local minimum thickness at vulnerable features?
- Are the thickness values tied to a stated measurement method and location map?
- Has the coating been evaluated alongside contact resistance and corrosion behavior, rather than thickness alone?
- Does the document say how rework, scratches, or handling marks are judged?
These are not administrative details. They are the difference between a thickness specification that can support long-term PEM stack review and one that only looks acceptable during document exchange.
Closing perspective
For corrosion resistance in PEM service, titanium bipolar plate coating thickness specifications work best when they are treated as a functional window, not a standalone number. The useful range is the one that keeps the conductive barrier continuous on real geometry, remains compatible with low contact resistance, and can be verified in a repeatable way. If you are evaluating plates for a hydrogen application and the thickness language feels vague, that hesitation is worth listening to. Tightening the specification before procurement is usually far easier than explaining stack degradation later.
Related News
- Hydrogen Energy Storage for Data Centers Gets Costly FastApr 27, 2026Hydrogen energy storage for data centers gets costly fast as hydrogen storage, cryogenic liquid hydrogen, safety standards, and utility-scale power needs reshape the energy transition case. Learn the real trade-offs.
- How hydrogen purity specification affects fuel cell performanceAug 25, 2026Hydrogen purity specification directly shapes fuel cell efficiency, durability, and warranty risk. Learn how trace contaminants impact PEM performance and lifecycle cost.
- Titanium Bipolar Plate Coating Thickness Specifications for Corrosion ResistanceAug 14, 2026Titanium bipolar plate coating thickness specifications are critical for corrosion resistance, low contact resistance, and PEM stack reliability. Learn how to define the right range and avoid costly failures.
- Zero-Carbon Infrastructure Projects: Where Stationary Fuel Cells Fit BestJul 11, 2026Zero-carbon infrastructure projects need reliable, low-emission power. Discover where stationary fuel cells fit best for data centers, ports, industry, and resilient remote sites.
Related News
- 00
0000-00
Hydrogen Energy Storage for Data Centers Gets Costly Fast - 00
0000-00
When 99.999% Hydrogen Purity Still Is Not Good Enough - 00
0000-00
When Does a Hydrogen-Ready Gas Turbine Pay Off? - 00
0000-00
Electricity Price Volatility Is Rewriting Hydrogen Cost Models - 00
0000-00
PSA Recovery Rate Drops for Reasons Operators Miss
Dr. Hideo Torque
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.